Formula details
Product Details
Overview
Technical Specifications: RTU Vials & Modular Systems
We manufacture our rtu containers and rtu vials under strict cleanroom conditions to ensure seamless integration into high-speed filling lines. Every modular vial system we produce adheres to global pharmacopeial standards, combining advanced polymer technology with ultra-tight dimensional tolerances.
| Specification Category | Technical Parameters & Standard Compliance |
|---|---|
| Product Formats | RTU Vials, RTU Containers, Nest & Tub Systems, Modular Vial Trays |
| Material Options | Medical-Grade COP, COC, PP, PE, PETG, PS |
| Regulatory Compliance | USP Class VI medical plastic, European Pharmacopoeia (EP), Japanese Pharmacopoeia (JP) |
| Manufacturing Standards | Precision injection molding up to ±0.02 mm tolerance in ISO Class 7 & Class 8 Cleanrooms |
| Quality Control | Automated optical inspection (AOI), continuous particulate monitoring, bioburden testing |
| Thermal Limits | Deep cryogenic and cold-chain storage compatible |
Core Engineering Standards
- Ultra-Tight Tolerances: High-precision injection molding down to ±0.02 mm eliminates dimensional variation, preventing line jams during automated robotic picking.
- Advanced Polymer Barrier: High-clarity Cyclic Olefin Polymer (COP) and Copolymer (COC) deliver glass-like transparency with zero risk of breakage and superior drug stability.
- End-to-End Cleanroom Control: Produced entirely within ISO Class 7 and Class 8 cleanroom environments to enforce low-particulate counts and strict bioburden control.
To ensure your primary packaging matches secondary containment requirements, integrate these components with our custom vial packaging design with inserts and compliance tailored to your specific drug product needs.
End-to-End Custom Packaging Development
We engineer custom packaging solutions from initial drug compatibility testing to full-scale cleanroom manufacturing. Whether deploying standard rtu vials or a fully customized modular vial system, our four-step development workflow ensures perfect alignment with your filling line.
4-Step Engineering Workflow
- Step 1: Application Consultation & Material Selection
We evaluate drug stability, light protection, and barrier requirements to pick the ideal polymer. Choose premium COP/COC for sensitive biologics and gene therapies, or cost-effective PP and PETG for standard parenteral formulations. - Step 2: 3D CAD Modeling & Tooling Design
We design custom vial geometries and nest-and-tub configurations built specifically for your automated fill-finish line. Through our specialized in-house mold development, every rtu vial tray maintains exact mechanical alignment and zero surface defect standards. - Step 3: Rapid Prototyping & Sampling
Standard evaluation samples ship in 7–10 working days. For custom rtu containers requiring proprietary dimensional specs, our CAD-to-sample tooling delivers functional prototypes within 2 to 4 weeks. - Step 4: Cleanroom Mass Production & Quality Sign-Off
Every production run occurs in certified cleanroom environments with continuous environmental monitoring. You receive full batch traceability, dimensional inspection reports, and direct access to our technical support team for smooth regulatory filing.
- Step 1: Application Consultation & Material Selection
Development Timeline & Milestones
| Development Stage | Core Deliverables | Lead Time |
|---|---|---|
| Material & CAD Design | Polymer selection, 3D component modeling, line compatibility check | 3–5 Days |
| Prototype Sampling | Physical sample testing, nest/tub fit validation | 7–10 Days (Standard) / 2–4 Weeks (Custom) |
| Cleanroom Production | ISO cleanroom injection molding, automated optical scanning | Per Order Schedule |
| Quality Release | USP/EP/JP compliance documentation, batch inspection reports | Included with Shipment |
EU GMP Annex 1 Compliant RTU Manufacturing
We uphold strict contamination controls at every stage of production to guarantee that our rtu vials and modular vial system components meet demanding global sterility standards. We eliminate contamination risks directly at the molding phase to keep your aseptic lines running smoothly.
Cleanroom Production & Quality Standards
| Compliance Focus | Engineering & Process Control | Operational Impact |
|---|---|---|
| EU GMP Annex 1 Compliance | Anti-static polymer selection and low-particulate contact designs during transport and line feeding. | Dramatically reduces particulate risks on high-speed automated filling lines. |
| Strict Bioburden Control | Continuous air/surface sampling paired with 100% automated vision scanning systems. | Guarantees zero-defect batches for all rtu containers. |
| Guaranteed Tooling Ownership | Exclusive customer mold retention paired with complete lifecycle maintenance plans. | Protects proprietary container designs and secures long-term supply stability. |
Bioburden Control & Custom Tooling Security
We manufacture every rtu vial solution inside our ISO-certified cleanroom manufacturing facility to maintain total batch purity.
- Static & Particulate Reduction: Optimized container geometries prevent surface friction and particle generation during automated line un-nesting.
- Continuous Quality Scanning: Automated optical systems flag dimensional defects and surface particulates before final sealing.
- Dedicated Mold Retention: We maintain, repair, and store your custom tooling exclusively for your production requirements.
For complete integration details, integrate our solutions directly into your established pharmaceutical vial packaging process.
Streamlining Aseptic Fill-Finish Workflows with RTU Solutions
Transitioning to pre-sterilized primary packaging transforms your aseptic fill-finish processing line into a streamlined, high-yield operation. By integrating our rtu vials, pharmaceutical manufacturers eliminate non-core prep steps and drastically shorten time-to-market.
Eliminating In-House Washing & Depyrogenation
Processing unwashed components in-house drives up capital expenditure, operational TCO, and facility footprint. Our pre-cleaned, bioburden-controlled rtu containers arrive depyrogenated and sterile, directly optimizing your facility resources:
- Facility Footprint Reduction: Free up critical cleanroom space by removing water-for-injection (WFI) washing stations and energy-intensive depyrogenation tunnels.
- Lower Energy Utilization: Cut utility consumption and facility operational costs significantly by eliminating high-heat heat-treatment cycles.
- Reduced Operational TCO: Lower validation burdens, labor overhead, and equipment maintenance expenses with ready-to-fill primary packaging.
Secondary Contamination Prevention
Maintaining sterility between transport and line feeding is critical for drug safety. Our modular vial system relies on an advanced containment architecture designed to secure each rtu vial throughout transit and cleanroom handling:
- Zero Surface Contact: Standardized matrix configurations protect container integrity, eliminating cosmetic scratches, cracks, and particle generation.
- Secure Cleanroom Transport: Sealed outer barriers shield containers from external particulates during shipping and transfer into controlled environments.
- EU GMP Annex 1 Alignment: Engineered layouts minimize static charge and manual intervention risks during automated filling.
Application Versatility
Our pre-sterilized packaging portfolio supports a broad spectrum of sensitive formulations and specialized filling demands across the global healthcare landscape:
| Application Sector | Key Benefit |
|---|---|
| Biologics & Parenteral Formulations | Low-particulate, bioburden-controlled surfaces preserving complex molecule stability |
| Cell & Gene Therapies | Secure containment engineered for cryogenic and cold-chain stability |
| Diagnostic Reagents | Precision dimensional tolerances ensuring leak-proof sealing and accurate liquid delivery |
| Small-Batch Clinical Trials | Rapid line changeovers and flexible processing without component preparation delays |
Engineered Modular Packaging Architecture
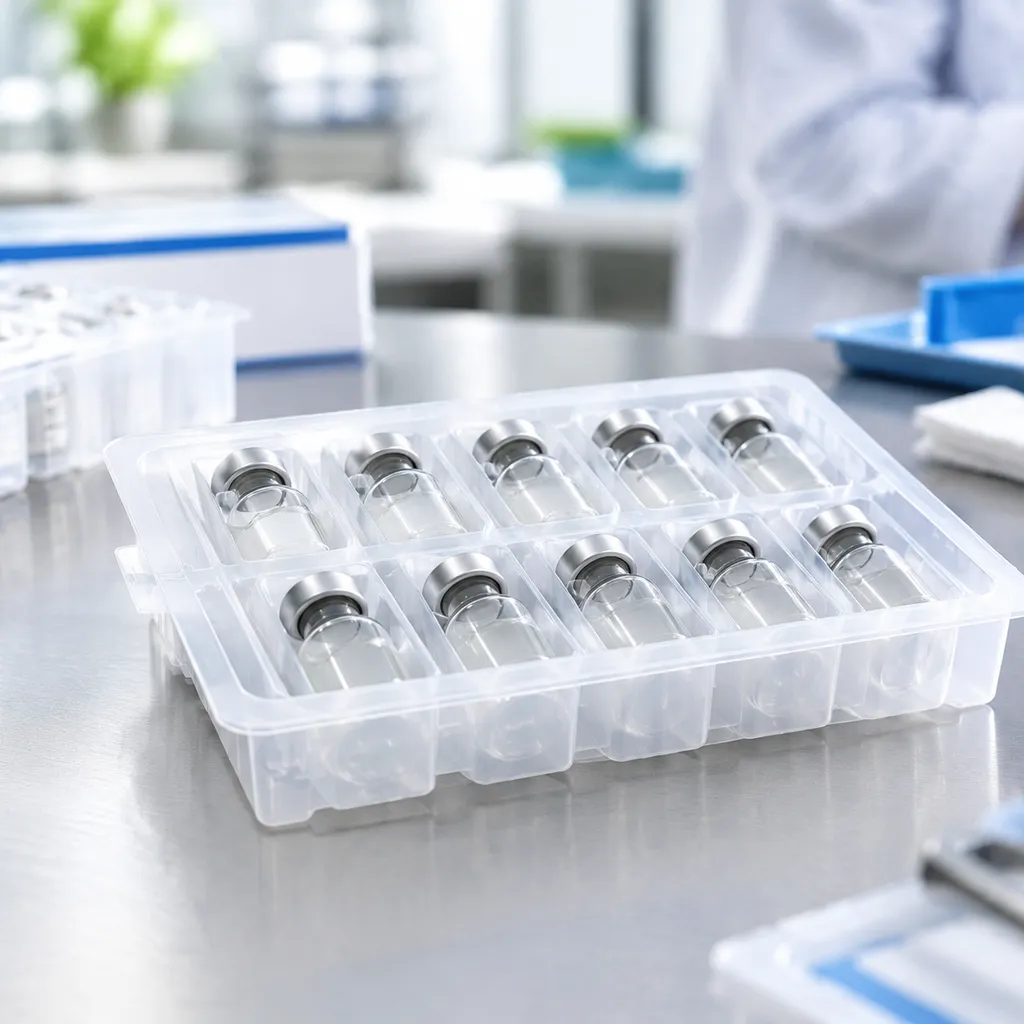
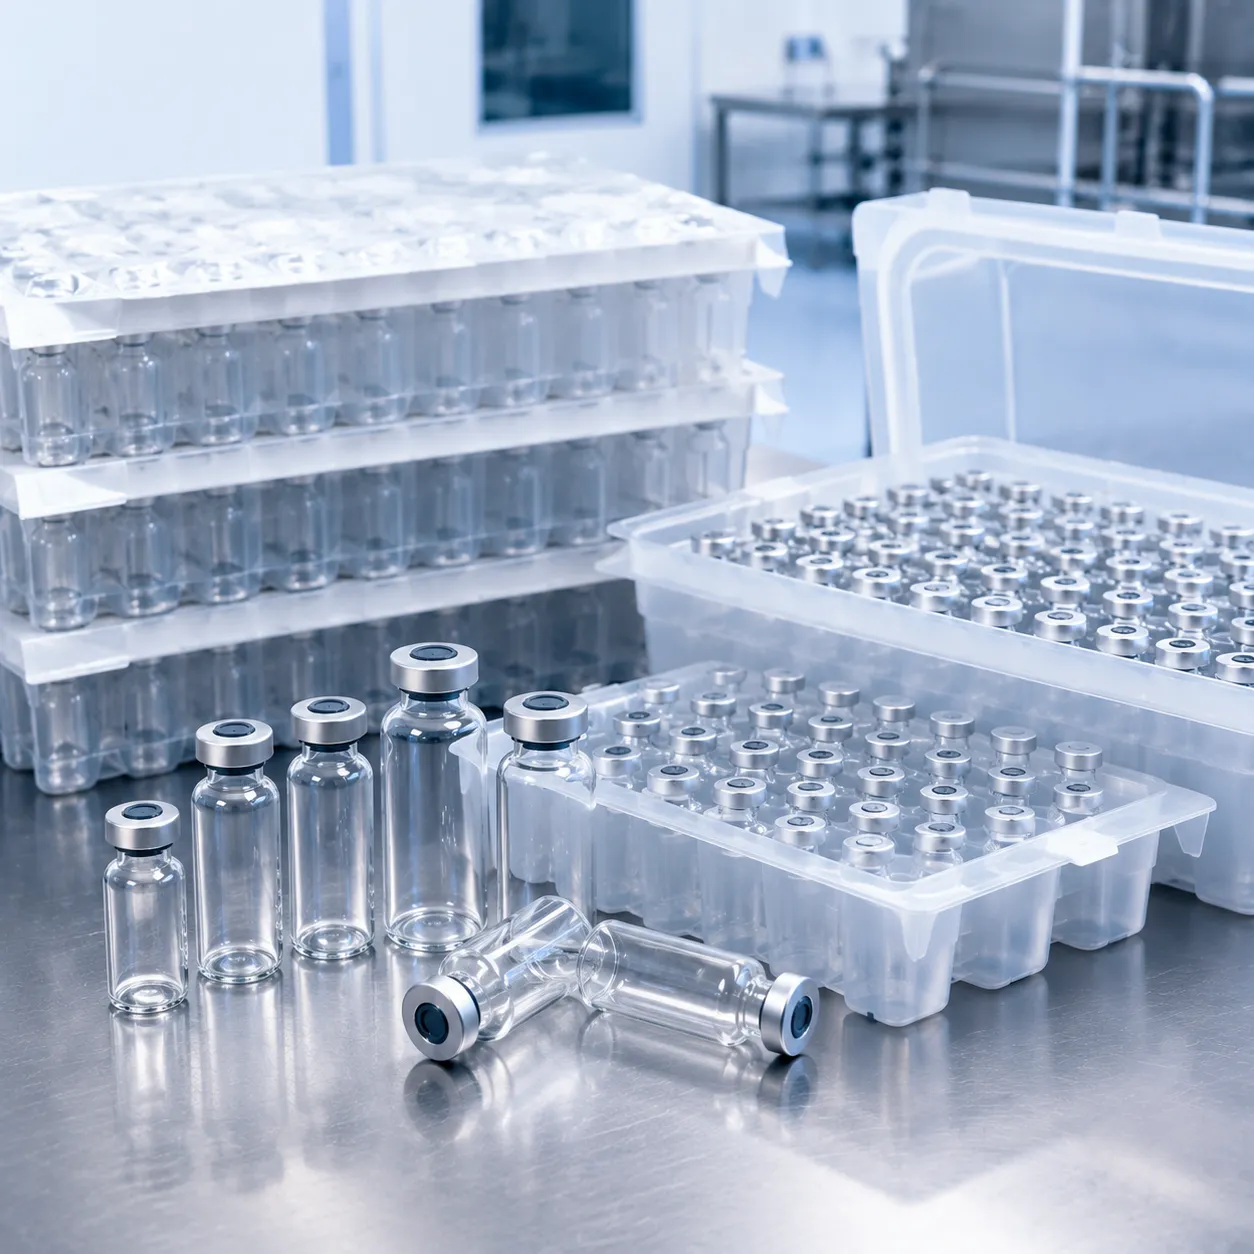
Traditional bulk packaging risks surface friction and particle generation during transit. Our pre-sterilized RTU containers utilize advanced nest and tub architectures to keep each unit secure, upright, and isolated throughout your entire workflow.
Nest & Tub Formats
- Zero-Contact Matrix Nests: Standardized nest design isolates each rtu vial, eliminating glass-to-glass and plastic-to-plastic contact to prevent cosmetic defects and particulate generation.
- Automated Line Compatibility: Engineered for smooth interfacing with robotic denesting and filling equipment, accelerating fill-finish processing without line stops.
High-Precision Modular Vial Trays
- Stable Robotic Handling: Custom-engineered plastic trays maintain rigid orientation during high-speed picking, significantly lowering mechanical jam rates.
- Secure Lab & Storage Systems: Durable secondary boxes protect product integrity across cold-chain and cryogenic environments. Explore our high-precision serum vial packaging boxes for optimized storage and transport stability.
Flexible Sizing Compatibility
- Standard & Custom Volumes: Accommodates standard ISO vial capacities from 2R up to 50R across diagnostic and pharmaceutical filling formats.
- Scalable Applications: Seamlessly transitions between small-batch clinical trials—utilizing specialized 2ml vial box storage options—and full-scale commercial manufacturing of RTU vials.
RTU Containers & Modular Vial Systems FAQ
Available Materials for Modular RTU Vial Systems
We engineer our modular vial system components using high-purity polymers, including Cyclic Olefin Polymer (COP), Cyclic Olefin Copolymer (COC), Polypropylene (PP), and Polyethylene (PE). All medical-grade resins comply strictly with USP Class VI, EP, and JP standards, guaranteeing minimal extractables and full chemical compatibility for sensitive biologics and parenteral formulations.
Integration with Automated Fill-Finish Lines
Our pre-sterilized rtu containers and nest and tub formats adhere to standardized packaging footprints. They integrate directly into modern automated aseptic fill-finish processing equipment, ensuring smooth robotic picking, de-nesting, and zero glass-to-glass contact without requiring modifications to your existing line.
Prototype and Standard Sample Lead Times
- Standard Sample Kits: Dispatched in 7–10 working days for quick evaluation.
- Custom Tooling & Prototypes: Delivered within 2 to 4 weeks following CAD design approval, backed by ISO Class 7 cleanroom injection molding with dimensional tolerances as tight as ±0.02 mm.
For clinical trial batches requiring specialized secondary protection, explore our custom 10ml vial box packaging with inserts to secure your primary containers during transport.
Batch Documentation for Regulatory Compliance
Every batch shipment of rtu vials includes a complete compliance package designed for effortless regulatory submission:
Certificate of Analysis (CoA) and Certificate of Conformance (CoC)
Continuous particulate, bioburden, and endotoxin test logs
Full raw material batch traceability reports aligned with EU GMP Annex 1 standards
Custom Designs for Non-Standard RTU Vial Dimensions
We routinely design custom rtu vial handling setups for unique geometries. Using in-house 3D CAD design and custom molding tools, we create tailored modular trays and specialized outer containment systems, including custom window vial boxes with inserts, to precisely fit your drug product specifications.