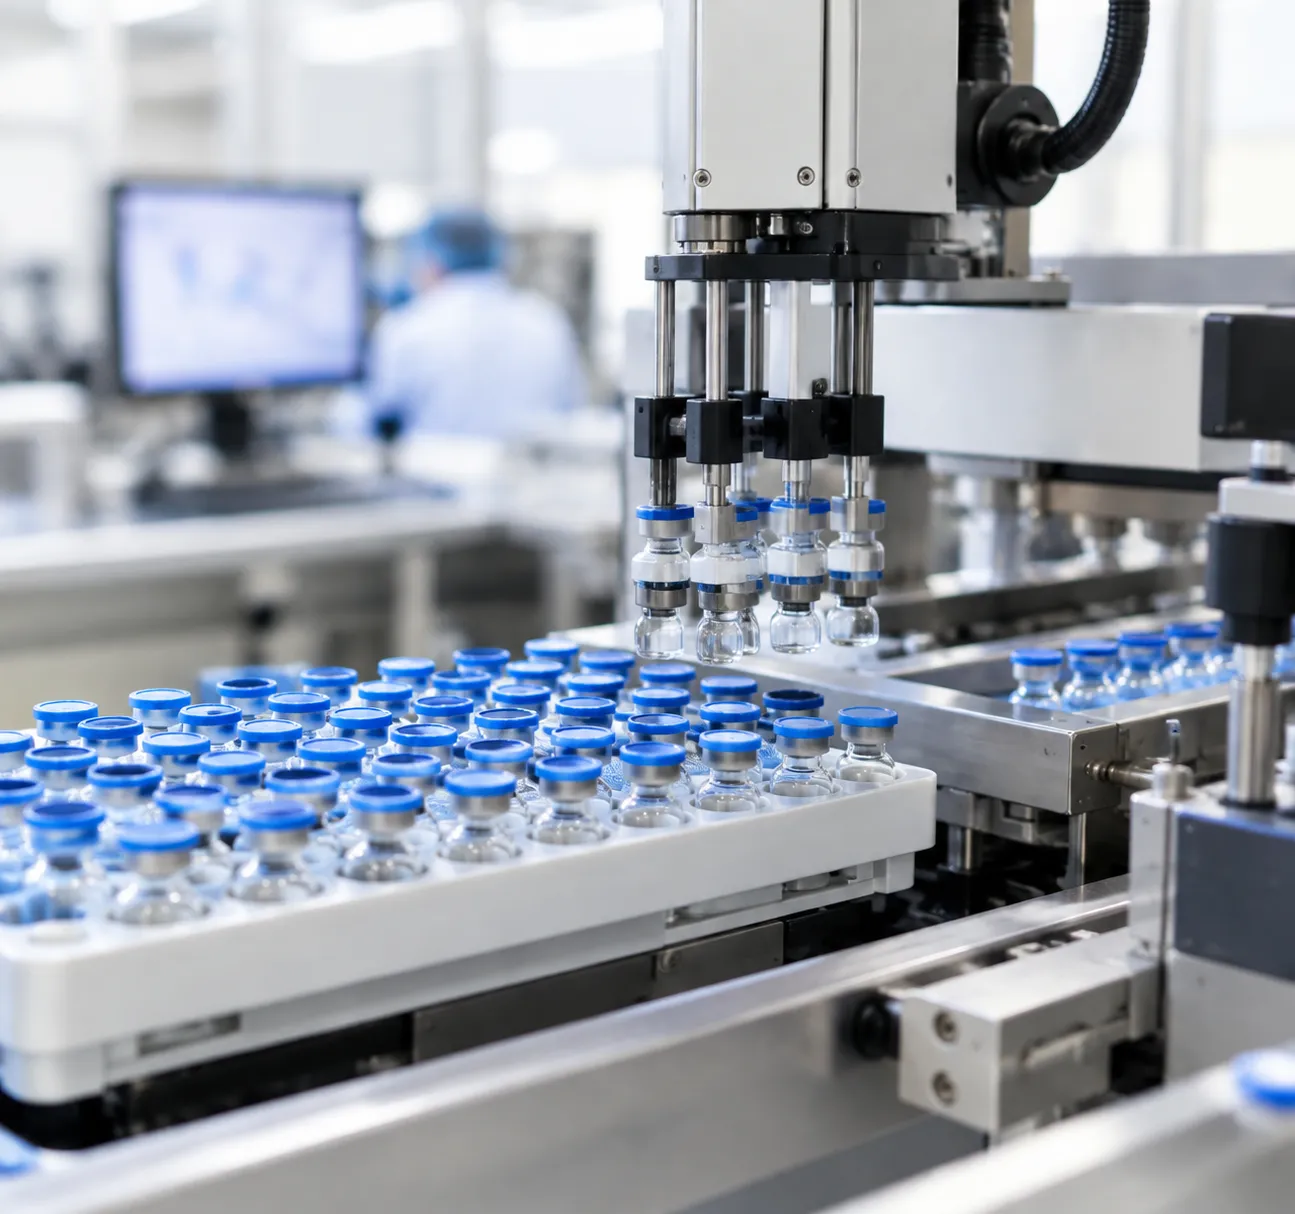
Types of Vial Tray Loading Systems
Manual Tray Loading Limitations and Contamination Risks
Relying on manual labor to load sterile vials into trays introduces significant operational vulnerabilities in modern aseptic vial handling:
- Particulate and Microbial Risks: Human intervention remains the primary source of cleanroom contamination, directly conflicting with Annex 1 standards.
- Tipping and Breakage: Fragile, lightweight containers (especially 2R and 4R formats) easily tip over during manual collation, generating costly product loss and glass shards.
- Throughput Ceilings: Operators struggle to keep pace with modern fill lines operating above 60 vials per minute, creating costly line stoppages.
Semi-Automated Vial Traying for Small-Batch Clinical Runs
For compounding pharmacies, pilot plants, and Phase I/II clinical trials, semi-automated traying provides a balanced compromise between cost and control.
These units use motorized conveyors and pneumatic pushers to collate a full row or matrix of vials. The operator simply loads an empty tray into the fixture, engages the cycle via foot pedal or optical sensor, and removes the filled tray. This mechanical push system eliminates direct glove contact with container bodies, ensures consistent push forces, and accommodates frequent format changes without dedicated robotics.
Fully Automated Servo-Driven and Robotic Pick-and-Place Loaders
For commercial-scale sterile fill-finish operations running from 120 to over 400 vials per minute, fully automated tray loaders eliminate operator presence within the critical core. We utilize two primary architectures based on spatial and throughput demands:
| System Type | Mechanism | Best Suited For | Key Operational Advantages |
|---|---|---|---|
| Servo-Driven Pusher | Continuous-motion accumulation table with multi-axis servo transfer arms | High-speed, standard run campaigns (60–400+ bpm) | High-speed linear transfer, simple mechanical tuning, maximum throughput |
| Robotic Pick-and-Place | 4-axis or 6-axis cleanroom-rated articulated arms with vacuum gripper heads | Multi-format lines, nested RTU vials, flexible arrays | Zero glass-to-glass contact, rapid digital recipe changeovers, minimal mechanical wear |
Our automated vial loading system configurations integrate seamlessly beneath isolators and Restricted Access Barrier Systems (RABS). Utilizing precision vacuum tooling and continuous-path servo kinematics, these loaders stabilize every container from infeed to final tray nesting without scuffing or micro-cracking.
Vial Tray Loading Mechanics and Packing Patterns
When we run high-speed fill-finish lines, moving vials from single-file mass flow into a stable tray matrix is where physical bottlenecks usually occur. Uncontrolled line pressure causes glass scuffing, micro-cracks, and tip-overs that trigger cleanroom interventions. Mastering vial tray loading requires pairing precise mechanical collation with the right packing geometry for downstream processing.
Orthogonal Grid Packing for Inspection and Autoclaving
Orthogonal packing sets vials into straight rows and columns with perpendicular 90-degree alignment. We use this layout when individual container visibility and robotic handling downstream take priority.
- Vision Inspection Clarity: Cameras can scan single containers across uniform sightlines without adjacent vials blocking shoulder or bottom curves.
- Autoclave Steam Penetration: The square gaps between vials permit balanced thermal circulation and moisture evacuation during terminal sterilization.
- Pick-and-Place Transfer: Standard Cartesian gantry and delta robots pick from orthogonal matrices using fixed-pitch vacuum or mechanical grippers without offset adjustments.
Hexagonal Honeycomb Packing for Lyophilization Thermal Transfer
Hexagonal packing offsets alternate rows by half a vial diameter, nesting each container into the pockets formed by the row ahead. This arrangement is essential for any high-capacity lyophilization tray loader.
- Maximized Shelf Real Estate: Honeycomb nesting packs 12% to 15% more vials into the exact same footprint compared to orthogonal grids.
- Consistent Heat Transfer: Uniform perimeter contact creates steady conduct between vials and freeze-dryer shelf surfaces, eliminating cold spots and batch sublimation drift.
- Structural Self-Support: Interlocking nesting stops top-heavy or tall vials from tipping during shelf loading inside the freeze dryer chamber.
Timing Screws, Starwheels, and Pressureless Accumulation
Pushing vials blindly against dead-plates to force a row pattern creates severe line backpressure. In modern aseptic vial handling, we rely on synchronized mechanical indexing to eliminate glass strain:
- Variable-Pitch Infeed Screws: Scroll timing screws gently widen container spacing, decelerating vials without abrupt hard-stop collisions.
- Servo-Driven Starwheels: Index single vials directly into transport lanes with zero lateral scuffing.
- Pressureless Infeed Decks: Multi-belt dynamic accumulation zones run speed-matched conveyor strips beneath the containers. The strips absorb kinetic energy, preventing container cluster pinch and glass dust shedding.
Bottomless, Solid, and Nested RTU Vial Formats
Tooling choices depend directly on how downstream processes interact with the vial base:
| Tray / Carrier Format | Primary Application | Handling Mechanism | Key Production Advantage |
|---|---|---|---|
| Bottomless Metal/Composite Frames | Freeze-drying (Lyophilization) | Sliding bottom plate retracts over freeze-dryer shelves | Direct vial contact with thermal shelves; frame lifts clear before cycle starts. |
| Solid Rigid Trays | Cold-chain storage, quarantine, and autoclaving | Fixed base carrying containers safely between workcells | High structural protection. Engineered plastic vial trays for pharma lab storage and transport withstand repeated wash cycles and temperature swings. |
| Nested Ready-to-Use (RTU) | High-value biologics and low-shear aseptic filling | Robotic pick-and-place into pre-molded polymer grids | Zero glass-to-glass contact. Adopting a dedicated vial nest and tub system for RTU aseptic fill-finish preserves cosmetic integrity and speeds up campaign turnovers. |
Critical Fill-Finish Challenges Solved by Vial Tray Loading
Maintaining Laminar Airflow in Isolators and RABS
Preserving unidirectional Grade A airflow inside Restricted Access Barrier Systems (RABS) and isolators is critical. Bulky mechanical pushers and solid plates disrupt air velocity, creating turbulence and dead zones that invite particulate accumulation.
- Aerodynamic Profiles: Modern tray loaders use slim, perforated pusher bars and skeletonized frames to allow vertical laminar air to sweep straight through.
- Minimal Footprint Drive Mechanics: We keep drive motors and belt mechanisms outside or below the sterile zone, running sealed shafts through barrier walls to maintain sterile fill-finish standards.
Preventing Glass-to-Glass Contact and Micro-Cracks
High line speeds often lead to container collisions. Glass-to-glass contact causes cosmetic scuffing, glass particulates, and invisible micro-cracks that compromise container closure integrity (CCI) during freeze-drying or terminal sterilization.
- Controlled Deceleration: Servo-driven loading fingers match vial speed dynamically, gently collating containers row by row without hard stops.
- Separated Row Pushers: Individual row pockets and indexed timing belts ensure glass containers never impact each other under line pressure.
| Risk Factor | Traditional Handling | Advanced Vial Tray Loading |
|---|---|---|
| Glass Micro-Fissures | High line pressure & impact | Individual pocket indexing |
| Particulate Shedding | Metal-on-glass friction | Certified polymer guide paths |
| Airflow Turbulence | Solid steel bulkheads | Perforated, low-drag tooling |
| Container Tipping | Free-standing inertia | Vacuum bottom-assist transport |
Non-Metallic Contact Materials for Sterile Vial Handling
Material selection across guide rails, scroll feeds, and pushers makes or breaks particulate counts:
- Medical-Grade Polymers: We engineer all direct-contact components from virgin PEEK, POM-C (Delrin), and PTFE to prevent container scratching.
- Chemical Resistance: These materials withstand aggressive CIP/SIP protocols, continuous vaporized hydrogen peroxide (VHP) cycles, and standard alcohol washdowns without degradation or leaching.
Stabilizing Small and High-Aspect-Ratio Vials at High Speeds
Slender containers—such as tall 2 mL to 10 mL formats outlined in our peptide vial sizes guide—have a high center of gravity. Rapid deceleration makes them prone to tipping, which causes catastrophic line jams.
- Vacuum Belt Transfers: Under-belt vacuum stabilization holds container bases firmly during collation, completely preventing base-wobble during lateral transfers.
- Continuous Top-Guide Rails: Spring-loaded overhead damping tracks secure the vial crimp neck through every transfer phase, allowing smooth, continuous vial tray loading at speeds exceeding 400 vials per minute.
Equipment Selection and Line Integration for Vial Tray Loading
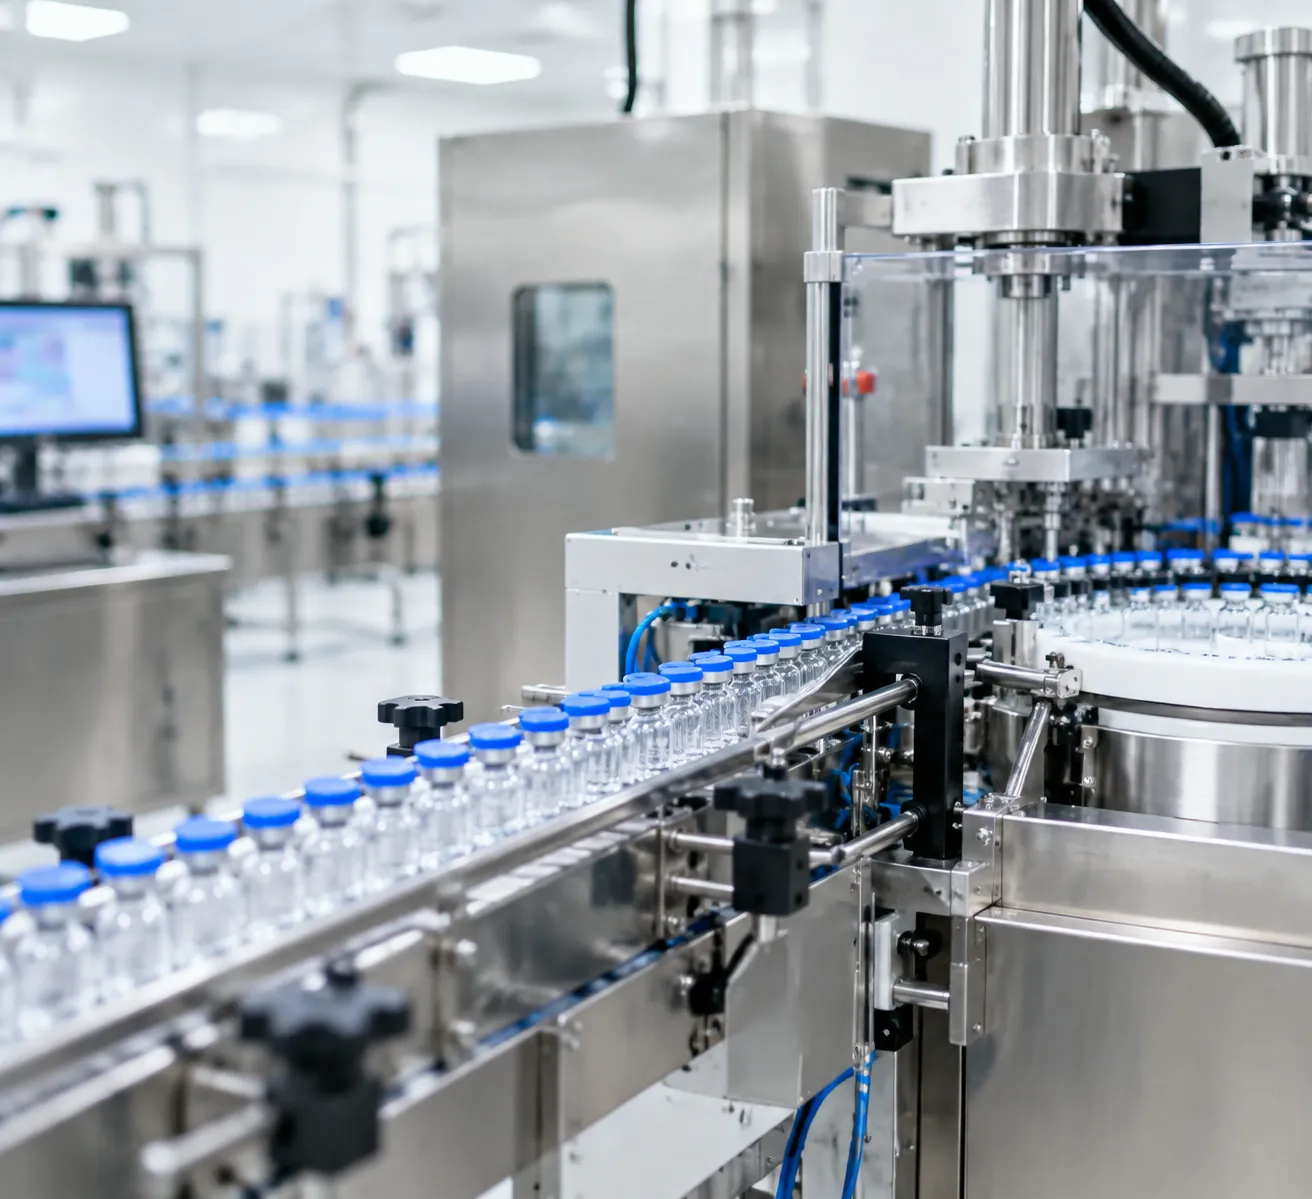
Integrating a new automated unit into an active sterile fill-finish line comes down to footprint, speed synchronization, and rapid turnarounds.
[ Upstream Filling / Capping ]
│
▼
[ Dynamic Buffer / Infeed ] ── (Real-time speed matching)
│
▼
[ Multi-Axis Tray Loader ] ── (Linear or 90° layout)
│
▼
[ Downstream Secondary Packaging / Lyophilization ]
Synchronizing Line Speeds: Upstream Filling to Downstream Traying
When upstream fillers push 200 to 400 vials per minute, even slight downstream hesitations cause line backpressure and glass clashing.
- Dynamic Infeed Buffers: We balance incoming flow with dynamic scroll-feed screws and servo starwheels to keep vials spaced evenly.
- Continuous Velocity Matching: Optical sensor arrays read line backlog in real time, automatically ramping the tray loader acceleration curves up or down to eliminate stop-and-go stutter.
- Zero Backpressure Collation: Low-friction conveyor zones stage full rows without crushing fragile containers.
Cleanroom Footprint: Linear vs. Right-Angle Layouts
Cleanroom floor space is expensive. Picking the right footprint layout ensures smooth personnel workflow and maintains clean laminar airflow patterns:
| Layout Type | Best Used For | Key Footprint Advantage |
|---|---|---|
| Inline (Linear) | High-speed, narrow continuous suites | Direct pass-through with minimal conveyor turns |
| Right-Angle (90°) | Compact cleanrooms and freeze dryer interfaces | Shortens total machine length and simplifies operator access |
| U-Shape Loop | Small-batch and clinical batch suites | Single-operator monitoring of loading and unloading zones |
Tool-Less Recipe Changeovers (2 mL to 100 mL Vials)
Switching batch recipes should not take your line down for hours. Our systems handle everything from small 2R vials to bulky 100R containers with minimal downtime:
- Quick-Release Change Parts: Color-coded guide rails, starwheels, and infeed funnels snap in without hand tools.
- Digital Recipe Management: Operators select the container format on the HMI screen, and servo drives automatically adjust pusher stroke, vacuum pick positions, and tray index depths in under five minutes.
- Repeatable Alignment: Precision dowel pins ensure zero drift during mechanical changeouts, preserving tight positional tolerances.
Integrating with Custom Secondary Packaging Solutions
Clean tray loading bridges sterile fill-finish with final cartoning, boxing, and distribution. We align loader discharge stations to feed directly into automated cartoning conveyors or custom secondary setups.
For high-value biologicals, pairing precise mechanical handling with a certified 2ml vial box for lab storage and serum packaging ensures zero container rattling during transport. Aligning our traying stations with dedicated custom vial packaging design with inserts guarantees smooth downstream transfers, prevents glass micro-fractures, and maintains full cGMP compliance from the cleanroom floor to cold-chain delivery.
Validation, Cleaning, and Maintenance Protocols for Vial Tray Loading
When an automated traying system drifts out of alignment inside a sterile cleanroom, production stops immediately. In our experience on the fill-finish floor, unexpected downtime during vial tray loading usually traces back to skipped predictive checks or incomplete validation. Keeping equipment running at peak speeds requires tight qualification protocols, rugged decontamination-ready designs, and proactive component monitoring.
Executing IQ/OQ/PQ Protocols for Positional Accuracy
Validating a servo-driven tray loader demands proof that the machine places vials into trays repeatedly without mechanical stress or misalignments. We break our qualification process into three clear phases:
- Installation Qualification (IQ): We verify all physical dimensions, utility supplies (compressed air, vacuum, power), contact material certifications (316L stainless steel, medical-grade PEEK, POM-C), and calibration records for every servo motor and optical sensor.
- Operational Qualification (OQ): We test mechanical performance across all functional limits. This involves testing pick-and-place coordinates, checking emergency-stop sequences without dropped glassware, and running positional accuracy stress tests at varying line speeds.
- Performance Qualification (PQ): We run full-speed production trials using representative containers to evaluate true process capability. The goal is zero container tip-overs, zero cosmetic scuffing, and perfect row packing density across hundreds of consecutive cycles.
CIP/SIP Regimens and VHP Decontamination Compatibility
Aseptic traying equipment must withstand aggressive, daily sanitization cycles without structural degradation or chemical carryover.
- Sanitary Build Standards: All frame joints, guide rails, and pusher plates must feature sloped designs, minimal horizontal faces, and zero exposed threads to eliminate liquid pooling during Clean-in-Place (CIP) and Steam-in-Place (SIP) routines.
- VHP Chemical Resistance: Isolator-integrated tray loaders face concentrated Vaporized Hydrogen Peroxide (VHP) cycles weekly. We utilize 316L electropolished stainless steel and FDA-compliant polymers like PTFE and PVDF that resist oxidative embrittlement and blistering.
- Barrier Isolation Integration: The loading mechanism must maintain unbroken unidirectional airflow. Seamless alignment with nested tub and tray aseptic processing solutions keeps particulate counts well within ISO 5 / Grade A limits during continuous tray transfers.
Predictive Maintenance for Key Motion Components
Waiting for a mechanical failure inside an isolator guarantees expensive batch losses. We use targeted predictive monitoring on high-wear assemblies to keep operations running smoothly.
| Component | Monitored Metric | Target Inspection Interval | Preventive Action |
|---|---|---|---|
| Servo Drives & Belts | Current draw spikes, thermal load, belt tension | Weekly / Continuous PLC monitoring | Retension belts, recalibrate homing offsets, replace belts at first sign of tooth wear |
| Vacuum Suction Cups | Vacuum decay rate, lip elastomer elasticity | Daily pre-run inspection | Swap out suction cups showing hardening, micro-tears, or particulate buildup |
| Linear Guide Rails | Vibration signatures, rail play/runout | Monthly | Apply cleanroom-certified, food-grade grease; wipe off excess lubricant to prevent misting |
| Pneumatic Pushers | Stroke cycle time, pressure drop across seals | Bi-weekly | Re-seal cylinders showing pressure loss; align pusher heads to prevent side-load friction |
Addressing these wear points proactively protects the vial tray loading process from sudden mechanical jams, eliminates glass-to-glass shock, and preserves consistent line throughput batch after batch.
Next-Generation Innovations in Vial Tray Loading
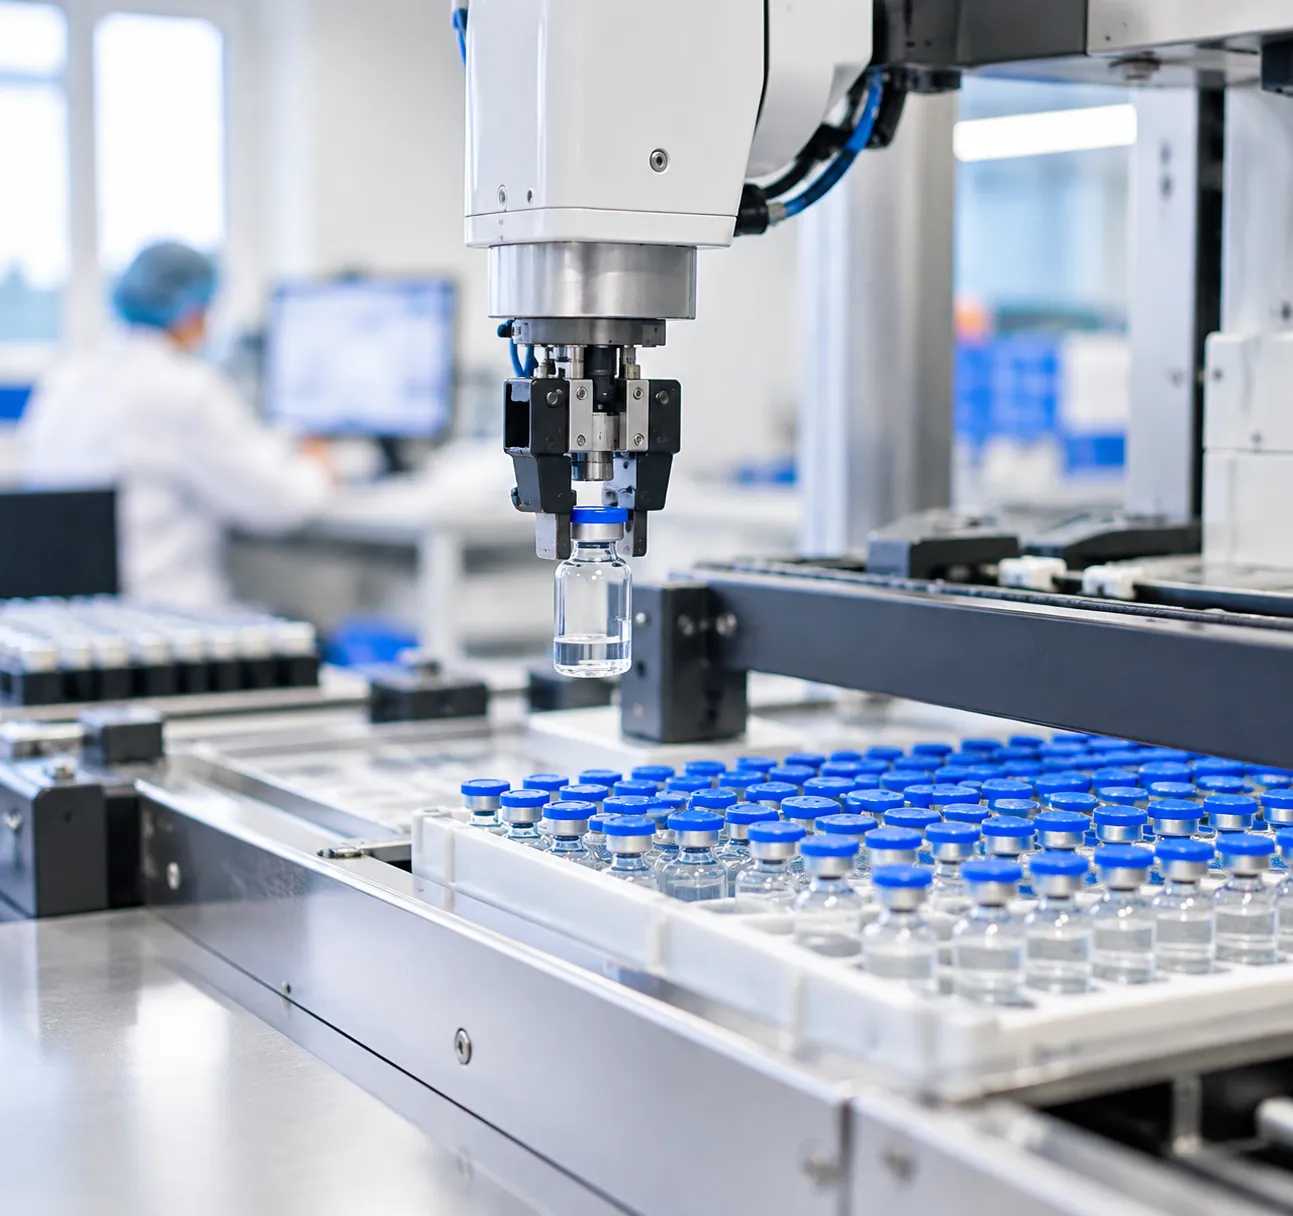
Traditional mechanical loaders have pushed physical limits for years. When handling 400 to 600 units per minute, mechanical guide rails, pushers, and standard belts hit bottlenecks: micro-scuffing, friction-induced particulate generation, and turbulence in laminar flow zones. To solve these friction points, modern sterile fill-finish operations are transitioning to smart sensing and frictionless transport.
Traditional Mechanical vs. Next-Gen Tray Loading
| Feature | Mechanical Infeed | Next-Gen AI & MagLev |
|---|---|---|
| Particulate Risk | Moderate (Belt/Guide) | Zero (Contact-Free) |
| Airflow Disturbance | High (Bulky Linkages) | Minimal (Planar Surfaces) |
| Defect Rejection | Post-Tray or Manual | In-Line Real-Time AI |
| Format Changeover | Mechanical Change Parts | Software Recipe Switch |
Vision-Guided AI for Real-Time Defect and Stopper Checks
Standard vision systems struggle with variable lighting, glass reflections, and high throughput speeds. We now integrate deep-learning vision systems directly upstream of the vial tray loading collation zone:
- Stopper Elevation and Skew Inspection: The system measures stopper seat depth and tilt angles instantly, flagging lyophilization stoppers that sit even 0.5 mm too high before tray entry.
- Real-Time Micro-Crack Detection: High-speed polarization cameras spot hairline fractures along the vial neck and heel, isolating compromised containers before the traying pusher exerts side pressure.
- Dynamic Defect Ejection: Defective units are diverted via starwheel blow-off without interrupting the incoming vial pitch, keeping downstream tray matrices intact.
Catching these container-closure integrity issues at the tray infeed prevents vial breakage inside freeze dryers. It also simplifies downstream processes, as outlined in our vial packaging process guide for pharmaceutical lines, where consistent tray arrays are critical for secondary packaging automation.
Contact-Free Magnetic Levitation in Grade A Aseptic Zones
Mechanical pushers and rotary tables generate friction and shed particles. In high-speed aseptic vial handling, we are replacing belts and chains with planar magnetic levitation (maglev) shuttles.
- Zero Particulate Generation: Shuttles float above sealed, smooth stainless steel surfaces using magnetic fields. There are no gears, lubricants, or belts to generate particulate matter inside the Restricted Access Barrier System (RABS) or isolator.
- Undisturbed Laminar Airflow: The flat profile of maglev movers allows sterile vertical laminar airflow to sweep cleanly over the open vials without creating vortices or dead zones.
- Individual Vial Motion Control: Instead of rigid timing screws, each shuttle operates as an independent servo axis. We group, space, and collate vials on the fly, shifting between orthogonal rows and hexagonal nesting via pure software commands.
These advancements transform vial tray loading from a mechanical risk point into an ultra-clean, data-driven step in modern sterile manufacturing.
Frequently Asked Questions About Vial Tray Loading
We run into the same practical questions every week when troubleshooting fill-finish suites and configuring automated traying lines. Here are direct answers to the technical concerns cleanroom engineers face on the floor.
What is the difference between orthogonal and hexagonal vial packing?
The difference comes down to geometry, thermal transfer, and floor space.
- Orthogonal (Grid) Packing: Aligns vials in square, straight rows and columns. It makes visual inspection, downstream carton packaging, and pick-and-place robotics simpler because every vial sits on an exact X-Y coordinate. However, it leaves substantial empty space between containers.
- Hexagonal (Honeycomb) Packing: Nests every alternate row into the gaps of the row ahead. This arrangement maximizes container density per square foot and delivers uniform surface-to-surface contact.
| Feature | Orthogonal (Grid) Packing | Hexagonal (Honeycomb) Packing |
|---|---|---|
| Packing Density | Standard (~78% surface utilization) | Maximum (~90% surface utilization) |
| Best Application | Visual inspection, autoclaving, secondary cartoning | Lyophilization (freeze drying) chambers |
| Thermal Uniformity | Moderate edge effects | Superior radiation and conduction balance |
| Handling Complexity | Simpler row-by-row pushing | Requires staggered row collation mechanisms |
How does automated tray loading prevent glass micro-cracks and particulate contamination?
High-speed glass-to-glass collisions cause cosmetic scuffing, micro-fissures, and sub-visible glass particulates that compromise product sterility. Automated systems eliminate these issues through three mechanics:
- Zero-Pressure Accumulation: Upstream timing screws and bi-directional buffer belts match filling speeds smoothly, eliminating the bottle-to-bottle head pressure that crushes thin-walled glass.
- Non-Metallic Contact Surfaces: Contact tooling uses medical-grade PEEK, Delrin, or ultra-high-molecular-weight polyethylene (UHMW-PE) instead of bare stainless steel to cushion every push stroke.
- Precision Nesting: Loading directly into custom-engineered vial tray formats isolates each container, eliminating friction during transit across the cleanroom barrier.
Can a single vial tray loader handle multiple vial sizes from 2R to 100R?
Yes, modern servo-driven tray loaders run across wide diameter ranges (from 16 mm up to 52 mm) on a single frame. We accomplish this flexibility through recipe-based automation and modular change parts:
- Tool-Less Changeovers: Quick-release starwheels, scroll infeed screws, and guide rails swap out in under 15 minutes without hand tools.
- Servo Stroke Profiling: Operators select the vial recipe on the HMI, and the pusher automatically shifts stroke length, deceleration curves, and row depth to match 2R or 100R footprints.
- Universal Deck Integration: The system handles standard bulk glass alongside pre-sterilized RTU vials by swapping out the collating pusher for nested nest-and-tub handling end-effectors.
How do tray loaders integrate with freeze dryer shelves?
A lyophilization tray loader functions as the critical link between the liquid filling zone and the freeze dryer chamber:
- Collation: The machine collates partially stoppered vials into tight hexagonal patterns on an open staging platform.
- Bottomless Tray Transport: Most high-output setups use frame-only (bottomless) trays or pusher bridge bars. This design pushes the nested vial pack directly onto the freeze dryer shelf without placing metal tray bases between the shelf and the vial bottoms.
- Direct Shelf Contact: Eliminating the tray base maximizes direct thermal conduction between the temperature-controlled lyo shelf and the drug product, cutting cycle times and keeping freeze-drying consistent across the batch.
What cleanroom standards apply to sterile vial tray loading systems?
Sterile vial tray loading systems must operate under strict cGMP requirements:
- EU GMP Annex 1 Compliance: The loading deck must fit within Grade A zones under continuous unidirectional laminar airflow (0.36 to 0.54 m/s).
- Aerodynamic Profiles: Guide bars, transfer arms, and pusher heads feature slim, sloped geometry and perforated surfaces to minimize air turbulence and prevent stagnant dead zones over open or partially stoppered vials.
- Isolator and RABS Compatibility: Drives, electrical actuators, and cabling sit isolated beneath the machine deck. All product-contact materials must endure repeated Vaporized Hydrogen Peroxide (VHP) decontamination cycles, aggressive clean-in-place (CIP) chemicals, and SIP exposure without pitting or degrading.