Formula details
Product Details
Overview
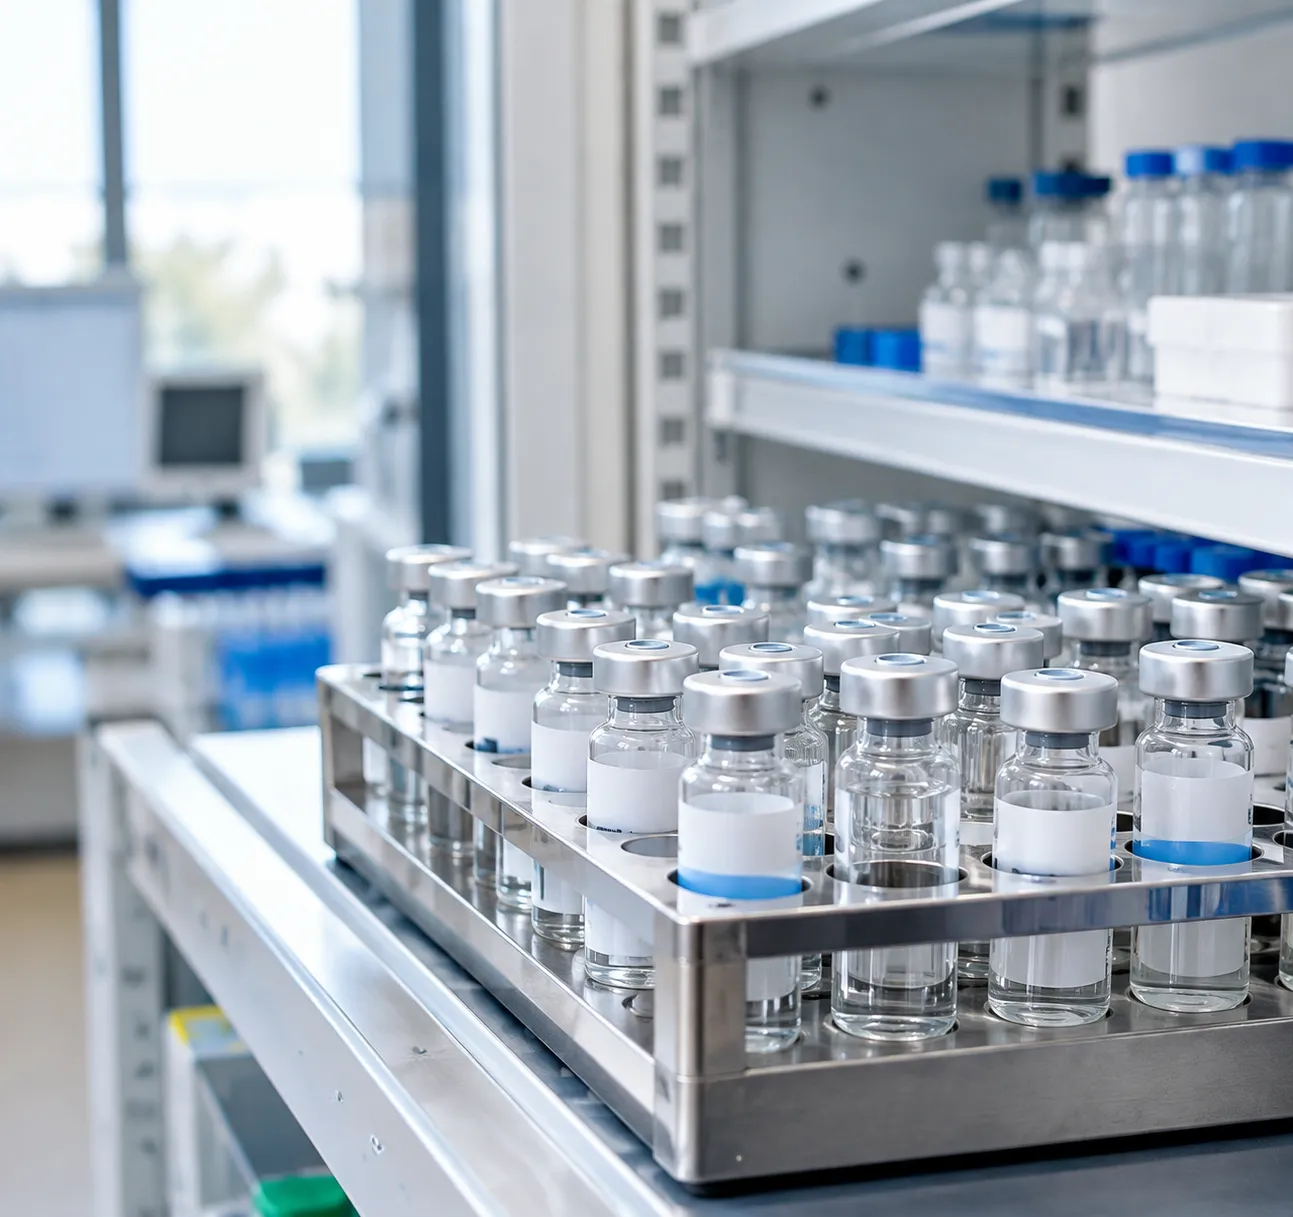
Industrial-Grade Pharmaceutical Vial Racks
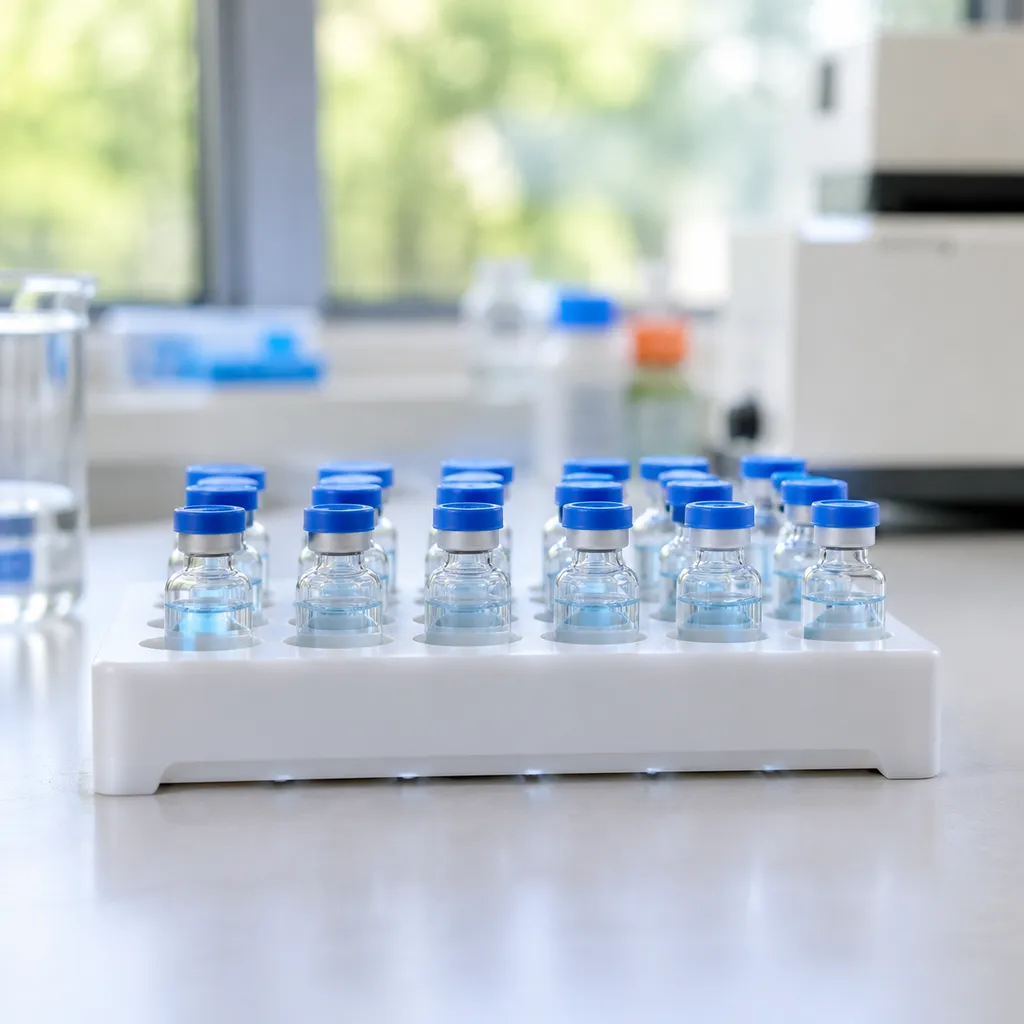
We manufacture industrial-grade pharmaceutical vial racks engineered to secure critical drug formulations, diagnostic reagents, and active biologicals across demanding production environments.
Preventing Vial Tipping, Surface Contamination, and Liquid Spills
Unstable glassware compromises sterile areas and leads to expensive sample loss. Our pharmaceutical vial rack design stabilizes containers at every stage:
- Low-Center-of-Gravity Cavities: Deep-well geometry firmly holds glass and plastic containers upright to eliminate accidental tip-overs during high-speed manual transfer.
- Elevated Base Profiles: Wells keep vial bases elevated above work surfaces, preventing direct contact with benchtop condensate or residual chemical films.
- Spill Containment Geometry: Perimeter borders help localize minor drips, stopping chemical migration across clean benches and biological safety cabinets.
Withstanding Repeated Autoclaving Cycles, Gamma Radiation, and Chemical Sanitizers
Sterility assurance requires labware that survives rigorous, repeated decontamination protocols without structural fatigue:
- Thermal Durability: Fully autoclavable vial rack engineering tolerates standard steam sterilization cycles (121°C at 15 psi) without warping, cracking, or dimensional shrinkage.
- Irradiation Stability: Resins withstand gamma and E-beam radiation processing without discoloration or polymer embrittlement.
- Aggressive Chemical Resistance: Complete inertness against daily wipe-downs with 70% IPA, sporicidal agents, quaternary ammonium compounds, and hydrogen peroxide vapor (HPV).
Precision Cleanroom Injection Molding to Eliminate Particulate Contamination
Particulate load directly impacts pharmaceutical batch yield. We manufacture every polypropylene vial rack within controlled cleanroom environments to deliver defect-free labware:
- Medical-Grade Tooling: High-polish, mirror-finish injection molds eliminate micro-burrs, flash, and rough seams that could scrape vial labels or shed plastic flakes.
- Zero Mold-Release Agents: Molded without heavy slip agents, plasticizers, or external lubricants, protecting your workflow against extractables and leachables.
- Particulate Control: Manufactured and bagged under strict environmental monitoring to meet ISO cleanroom standards, ensuring immediate compatibility with aseptic transfer zones.
Technical Specifications & Dimensional Matrix
Materials and Thermal Performance
We build our racks using medical-grade virgin polypropylene (PP) and impact-modified polycarbonate (PC). Both polymers remain fully inert and dimensionally stable across a wide working window:
Operating Range: Stable from -86°C cryogenic deep freeze up to 121°C steam autoclaving (15 psi for 20 minutes).
Thermal Transfer: Slotted base geometries promote uniform gas and liquid flow, speeding up freezing stages and complete drainage during washdowns.
Surface Quality: Precision-polished, burr-free mold cavities eliminate sharp friction points, protecting delicate paper and synthetic container labels from tearing during high-throughput loading.
For combined staging and bulk movement setups, our plastic vial trays for pharma lab storage and transport deliver the same uniform thermal and chemical stability across larger production runs.
Standard Layout & Sizing Matrix
To accommodate common fill-finish, storage, and analytics workflows—including standard dimensions detailed in our peptide vial sizes guide (2ml, 3ml, 5ml, and 10ml)—we offer multiple standard grid formats:
| Specification Parameter | Standard Configuration | Details & Options |
|---|---|---|
| Well Count | 24, 48, 50, and 96 wells | Optimized for standard bench spaces and automated decks |
| Vial Diameter Range | 11 mm to 45 mm OD | Compatible with 2 ml, 10 ml, 20 ml, and 50 ml+ serum vials |
| Polymer Base | Virgin Polypropylene (PP) / Polycarbonate (PC) | Heavy-metal free, low-extractable, USP Class VI compliant |
| Temperature Tolerance | -86°C to +121°C | Autoclavable, freeze-thaw resistant, vapor-phase LN2 safe |
| Base Configuration | Open-grid / Slotted drainage | Accelerates thermal transfer; prevents liquid pooling |
| Cavity Finish | SPI A2 mirror polish | Non-abrasive, burr-free contact surfaces protect labels |
Key Functional Features for Sterile Workflows
Performance and Design Matrix
| Feature | Technical Specification | Operational Benefit |
|---|---|---|
| Alphanumeric Indexing | Molded-in laser-sharp coordinate grid (A–H, 1–12) | Eliminates sample mix-ups and integrates directly with LIMS workflows. |
| Interlocking Footprint | Recessed top rim with anti-slip base lugs | Secure vertical stacking inside laminar flow hoods and biosafety cabinets. |
| Ventilated Base Wells | Open-bottom drainage and cross-flow channels | Facilitates uniform vapor transfer during lyophilization and flash freezing. |
| Chemical Inertness | Pure virgin polypropylene (PP) / polycarbonate (PC) | Non-leaching build resistant to DMSO, phenol, chloroform, ethanol, and acids. |
Error-Free Sample Tracking & Hood Optimization
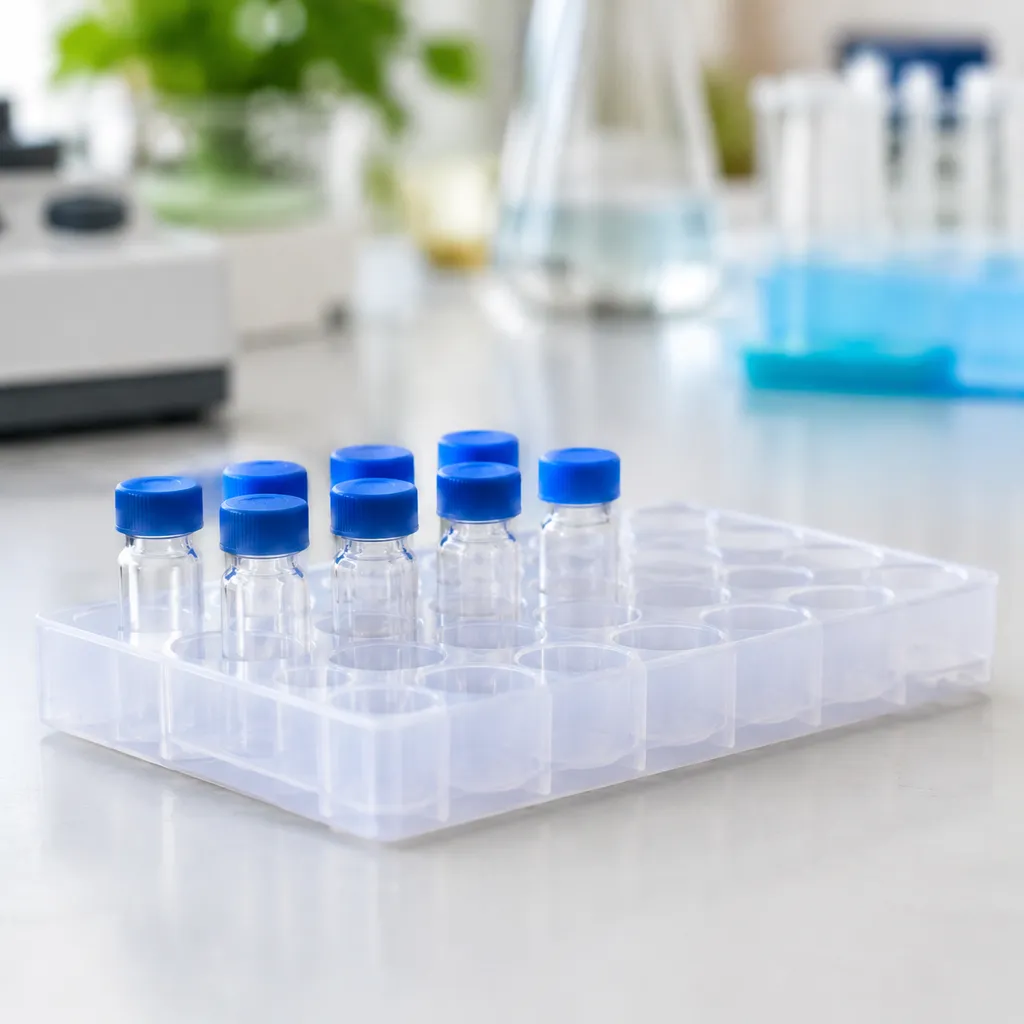
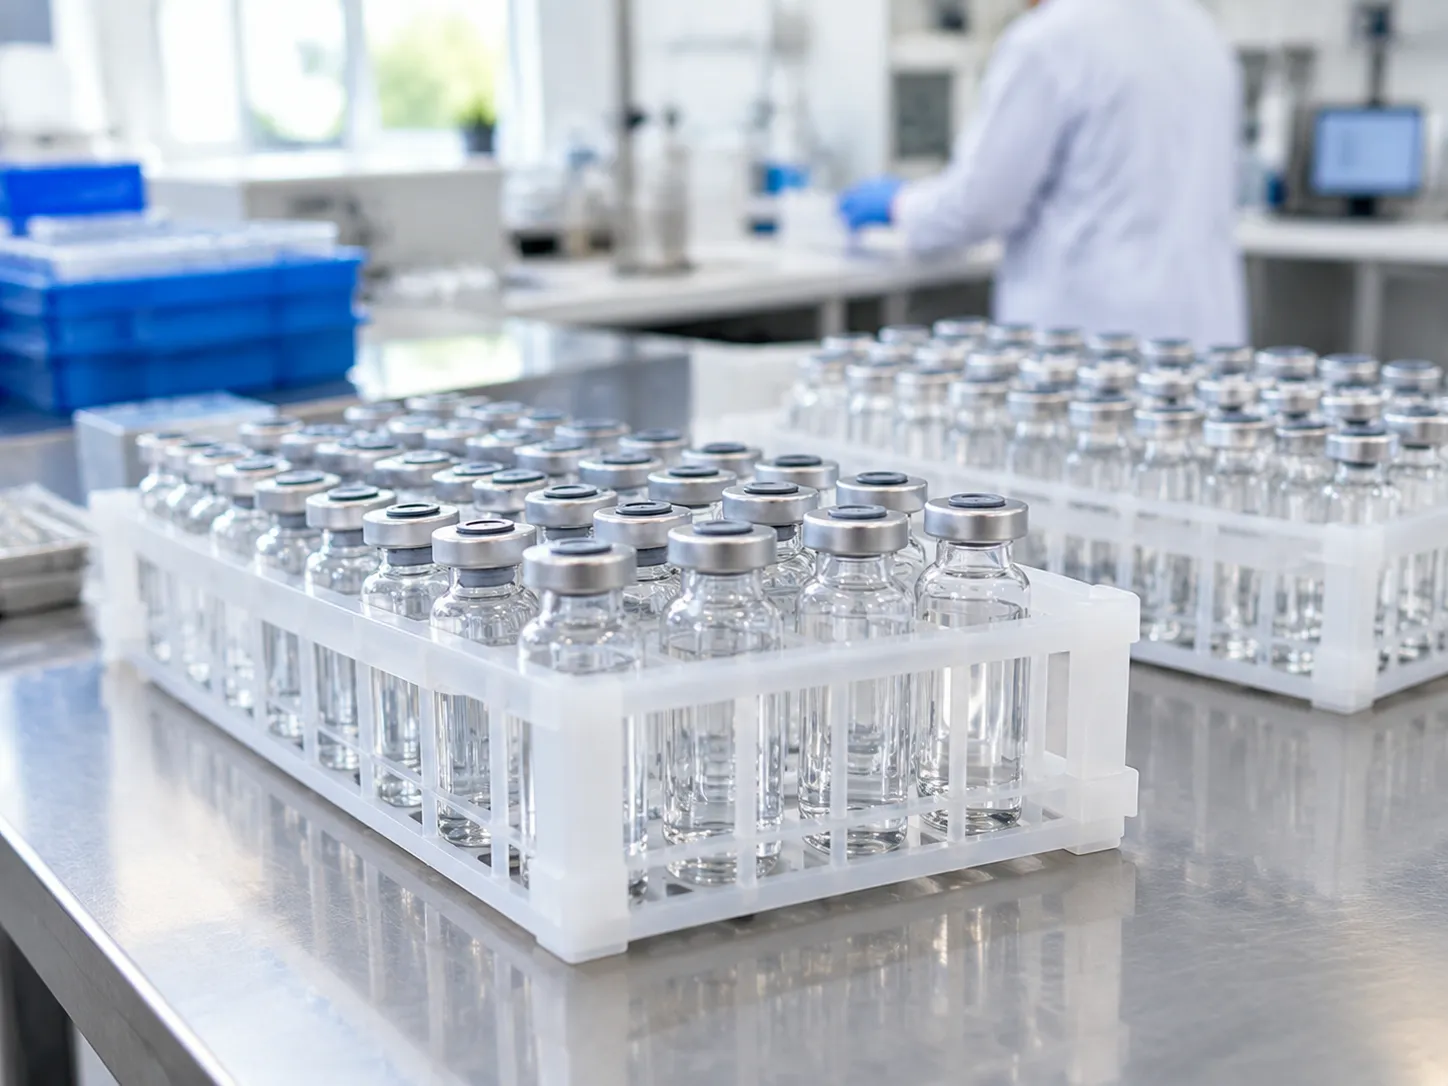
Every alphanumeric sample rack features high-contrast, permanent coordinates along both axes. This allows operators to quickly locate, log, and process target aliquots without misidentification risks.
To maximize restricted workspace, the stackable architecture stabilizes nested tiers during staging. When moving bulk batches between processing suites, our racks work seamlessly alongside sterile pharmaceutical trays for safe drug handling to keep your cleanroom staging organized and compliant.
Thermal Transfer and Chemical Durability
- Fast Gas and Temperature Exchange: Slotted well bottoms ensure uninterrupted air and nitrogen circulation, preventing thermal gradients during lyophilization, dry-ice staging, and liquid nitrogen vapor storage down to -86°C.
- Leach-Free Protection: Our polypropylene vial organizer units contain zero plasticizers, heavy metals, or mold-release agents, preventing extractables and leachables from compromising your high-purity formulations.
Pharmaceutical and Biotech Applications for High-Performance Vial Racks
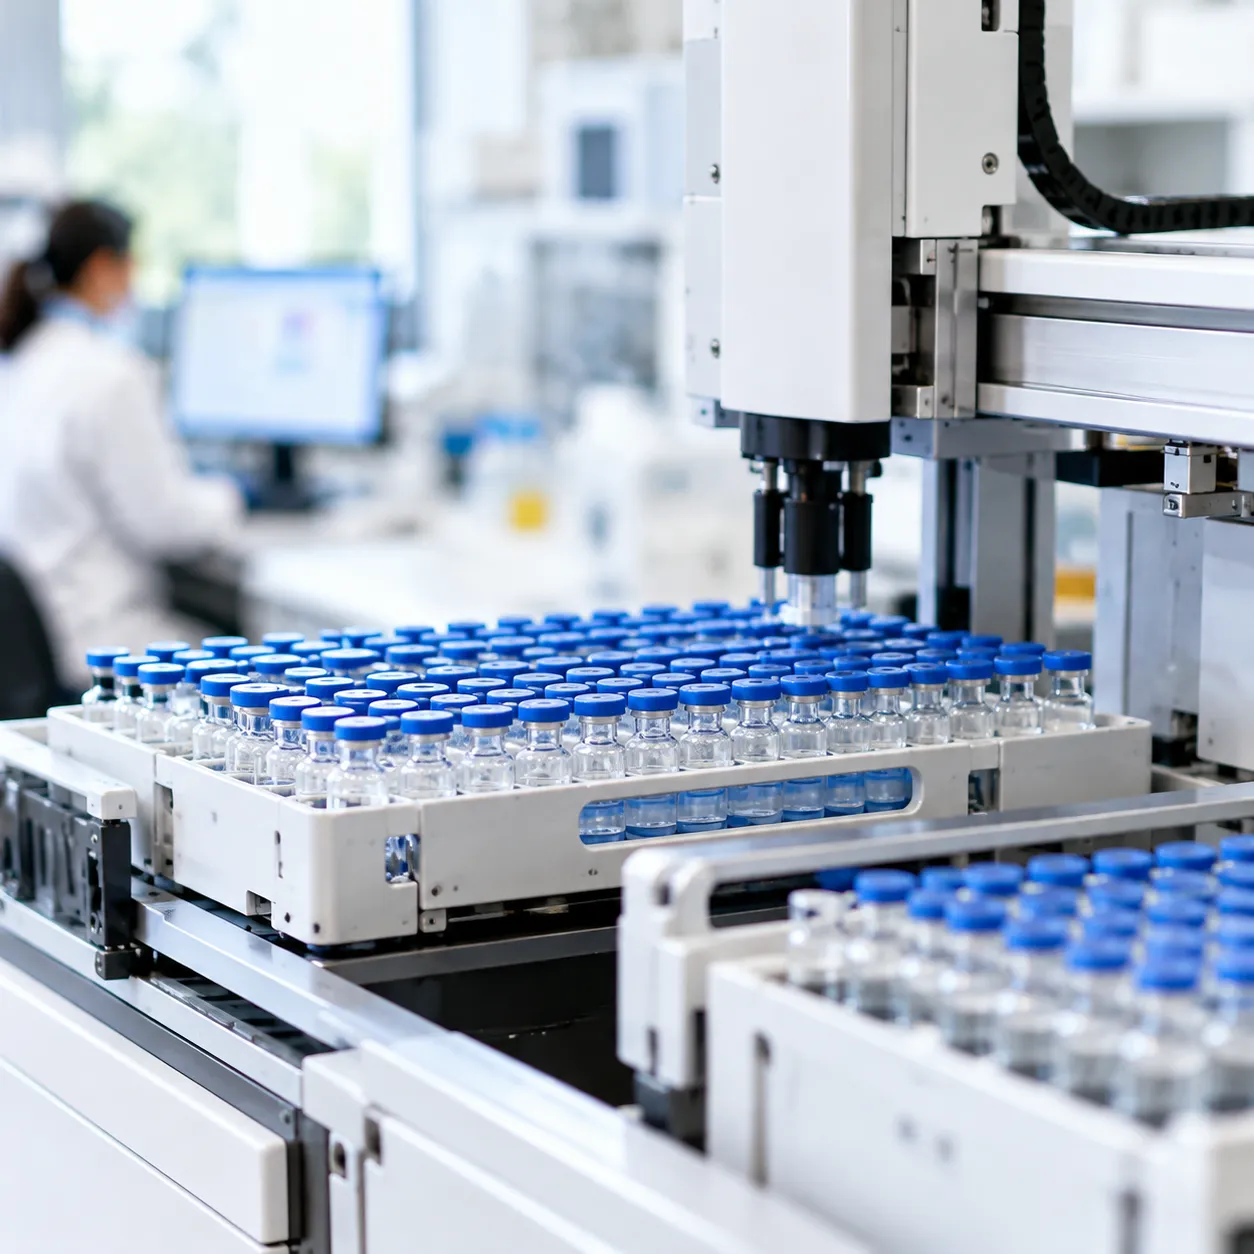
Our pharmaceutical vial racks integrate directly into regulated drug manufacturing, cleanroom packaging, and analytical testing environments.
Aseptic Filling, Capping Lines, and Weight-Check Staging
During aseptic processing, stability is critical to prevent product loss and airborne contamination.
Inline balance staging: Provides rigid support for gross and tare weight verification during high-speed fill runs.
Vial stabilization: Eliminates container tipping during automated stopper insertion and aluminum crimp capping.
Secondary packaging integration: Matches standard footprints, making it easy to transfer containers using our 10ml and 2ml vial box dimensions guide for optimized inventory and pack-out layouts.
Lyophilization Staging, Flash-Freezing, and Cryogenic Cold Storage
These vial storage trays are built for demanding thermal conditions, from blast freezers to freeze-dry chambers.
Open-grid base airflow: Promotes uniform sublimation rates during freeze-drying cycles.
Cryogenic resilience: Maintains full impact strength down to -86°C deep freeze storage without cracking or embrittlement.
Rapid flash-freezing: Allows liquid nitrogen vapor penetration for fast, even sample preservation.
Long-Term Stability Chamber Testing
For ICH stability testing programs (including 25°C/60% RH, 30°C/65% RH, and 40°C/75% RH):
Polymer durability: Resists continuous humidity and elevated temperatures without warping, dimensional warping, or leaching.
Sample integrity: Chemically inert surfaces prevent degradation of container labels, bar codes, or outer vial walls.
Robotic Sample Handling and Automated Liquid Handler Integration
Our precision-molded labware integrates seamlessly with robotic arms and deck systems.
| Automation Feature | Operational Benefit | Compatibility |
|---|---|---|
| Standard Footprint | Direct fit on deck surfaces | SBS-compliant platforms (Tecan, Hamilton, Beckman) |
| Rigid Well Tolerances | Accurate pipette tip alignment, zero lateral wobble | Multi-channel pipettes & robotic grippers |
| Chamfered Well Openings | Rapid, self-centering automated vial insertion | High-throughput filling and screening robots |
Custom OEM and ODM Manufacturing for Pharmaceutical Vial Racks
Standard labware does not always match specialized production lines or proprietary glass containers. As an experienced vial rack manufacturer, we engineer custom vial racks tailored precisely to your operational workflow, fill-finish machinery, and storage parameters. Whether you require unique well configurations or specialized polymer blends, our OEM and ODM services deliver ready-to-run solutions.
Custom Cavity Tooling for Non-Standard Containers
We design dedicated tooling to match non-standard diagnostic vials, lyophilization bottles, and tubular glass containers:
Tailored Cavities: Custom well diameters and depth profiles prevent loose play, container tipping, and neck stress.
Grip & Lock Options: Bottom-slotted snap locks and stepped well bases secure odd-shaped, conical, and skirted vials.
Integrated Packaging Workflows: Racks can be dimensioned to interface seamlessly with outer trays and transport boxes, matching requirements for custom vial packaging design with inserts and compliance.
Color Coding, Mold Embossing, and Lab Segregation
Visual management stops cross-contamination in busy cleanrooms. We customize the physical appearance and identification marks on every custom molded vial rack:
Medical-Grade Color Matching: Resins molded in high-visibility hues (blue, green, red, yellow, natural) to designate specific cleanroom suites, biohazard zones, or batch lots.
Direct Tool Embossing: Permanent cavity indexing, alphanumeric grid coordinates, tare weights, and chemical safety icons molded directly into the rack body.
Private Labeling: High-contrast laser etching and permanent in-mold branding for equipment distributors and diagnostic kit suppliers.
Rapid Prototyping to High-Volume Injection Molding
We shorten product development cycles with an agile manufacturing pathway:
3D CAD Modeling: Functional digital mockups built to your exact vial tolerances and robotic gripper clearances within 48 hours.
Rapid SLA/SLS Prototypes: Physical testing samples to verify fit, balance, and automation handling before steel cutting.
Multi-Cavity Hardened Steel Tooling: Precision production molds engineered for high-volume cleanroom injection molding, delivering consistent tolerances across millions of units.
Quality Assurance & Regulatory Compliance Standards
Certified Manufacturing Systems
- ISO 9001 Certification: Full operational adherence to documented quality controls, process consistency, and precision mold calibration.
- ISO 15378 Compliance: Specialized cleanroom manufacturing controls designed explicitly for primary packaging and direct-contact pharmaceutical materials, matching the integrity required for nested tub and tray aseptic processing solutions.
Raw Material & Biocompatibility Approvals
To eliminate leachables, extractables, and physical degradation, every polypropylene vial rack is molded exclusively from virgin, medical-grade resins tested against established regulatory benchmarks:
| Regulatory Standard | Scope & Verified Criteria |
|---|---|
| USP Class VI | Biocompatibility, systemic toxicity, and intracutaneous reactivity compliance |
| FDA 21 CFR 177.1520 | Olefin polymer compliance for safe chemical and drug-contact suitability |
| Heavy Metals & BSE/TSE | Free of animal-derived components, phthalates, BPA, and heavy metal additives |
Biological Purity & Lot Traceability
Our cleanroom vial organizers undergo systematic batch-release testing to protect cell cultures, active pharmaceutical ingredients (APIs), and sterile reagents. Each lot is certified:
- DNase & RNase Free: Undetectable enzyme presence preventing nucleic acid degradation.
- Non-Pyrogenic: Endotoxin levels verified below 0.05 EU/ml via LAL testing.
- Batch Documented: Shipped with comprehensive Certificates of Analysis (CoA) matching your specific audit and validation requirements.
Packaging Specifications, MOQ, and Global Logistics
We prepare every pharmaceutical vial rack shipment to meet strict pharmaceutical supply chain requirements. From cleanroom packaging to international freight management, our operations prevent bioburden introduction and transit damage.
Cleanroom Packaging for ISO Class 5–7 Transfer
Contamination control begins before our racks leave the plant. We pack each batch under controlled environments to simplify pass-through procedures into sterile suites:
- Double-Bagged Polyethylene Enclosures: Every cleanroom vial organizer is sealed in dual medical-grade bags. Operators wipe down and strip the outer bag in staging areas, preserving cleanroom air quality when transferring the inner bag into ISO Class 5–7 environments.
- Particulate-Free Cartons: Outer master cartons feature sealed seams and lint-free liners to prevent fiber migration into processing facilities. Understanding how container barriers interact aligns directly with the standards covered in primary vs secondary packaging for vials explained.
- Traceable Lot Labeling: Every carton includes barcode and QR-code labeling tied to production batch records, polymer material certifications, and QA release documents.
Minimum Order Quantities and Production Timelines
As a direct pharmaceutical vial rack manufacturer, we support commercial aseptic fill-finish lines, clinical research facilities, and contract packagers with flexible capacity:
| Order Classification | Minimum Order Quantity (MOQ) | Production Lead Time | Packaging Standard |
|---|---|---|---|
| Standard Stock Racks | 500 units | 3–5 business days | Double PE bagged, standard export master carton |
| Custom Color / Pad Printing | 2,000 units | 2–3 weeks | Double PE bagged, custom-labeled master carton |
| Custom Mold Tooling (OEM/ODM) | 5,000 units | 4–6 weeks (tooling + samples) | Cleanroom vacuum-sealed, palletized for air/sea |
Global Freight and Delivery Options
We manage domestic and international logistics across North America, Europe, and Asia-Pacific to maintain your production schedule:
- Air Freight (Priority & Standard): 3 to 7 business days for urgent line validations, stability studies, and rapid changeover requirements.
- Ocean Freight (FCL & LCL): Cost-effective bulk transport for routine inventory replenishments, secured on heat-treated ISPM-15 export pallets.
- Consolidated Freight & DDP Services: Full-service customs clearance and door-to-door delivery to simplify import processing for manufacturing sites.
Frequently Asked Questions: Pharmaceutical Vial Racks
Can pharmaceutical vial racks withstand standard autoclave cycles?
Yes. We manufacture our polypropylene vial rack units from high-purity, virgin medical-grade polymers. They handle repeated steam sterilization cycles at 121°C (250°F) at 15 psi for 20 to 30 minutes without warping, cracking, or degrading structural tolerances.
Are these racks compatible with automated liquid handling robots?
Our robotic liquid handling vial rack options adhere strictly to standard SBS/ANSI microplate footprint dimensions. The uniform well spacing, center-to-center pitch, and rigid outer walls ensure seamless integration with:
Automated pipetting and liquid dispensing heads
Robotic robotic-arm gripper systems
High-speed filling, capping, and inline optical inspection stations used throughout pharmaceutical vial packaging process lines
What is the chemical resistance profile against DMSO and ethanol?
The high-density polypropylene and engineered resins we use provide chemical inertness across common laboratory solvents and sanitizers:
Organic Solvents: 100% resistance to ethanol, isopropanol, DMSO, and methanol without surface clouding or leaching.
Sterilants & Cleaners: Resistant to hydrogen peroxide vapor (VHP), peracetic acid, and sodium hypochlorite solutions.
Acids & Alkalis: Stable against dilute acids, bases, and aggressive buffer solutions.
How do we order custom well dimensions for specialized containers?
We provide full OEM/ODM mold design for non-standard serum bottles, diagnostic tubes, and large containers:
1. Container Data: Share your container's outer diameter, base profile, and total height.
2. CAD Prototyping: Our engineering team generates 3D models with optimized drain holes and side-wall clearances.
3. Tooling & Sampling: We cut prototype injection molds for fit testing before releasing full multi-cavity production tooling.