Formula details
Product Details
Overview
Technical Specifications & Material Capabilities
ISO Cleanroom Injection Molding & Material Options
| Parameter | Engineering Standard | Operational Advantage |
|---|---|---|
| Environment | ISO Class 7 & Class 8 Cleanrooms | Prevents particulate contamination during production |
| Materials | USP Class VI Polymers (COP, COC, PP, PE, PETG, PS) | Ensures zero extractables/leachables impact on drugs |
| Tolerances | High-precision injection molding (up to ±0.02 mm) | Guarantees flawless robotic handling on automated filling lines |
| Defect Control | 100% Automated Optical Inspection (AOI) | Guarantees zero cosmetic or dimensional flaws |
Quality Assurance and Full Traceability
Our rtu parenteral packaging kits undergo rigorous testing to ensure seamless performance in critical drug delivery workflows:
- Medical-Grade Polymers: We utilize Cycloolefin polymer (COP) packaging trays and specialized resins for high chemical resistance and low bioburden.
- Continuous Monitoring: Production includes real-time airborne particulate counting and regular bioburden testing.
- Lot Traceability: Every shipment includes detailed Certificates of Analysis (CoA), dimensional inspection reports, and MSDS documentation.
- Custom Engineering: Designed to align with fully integrated custom vial packaging design with inserts for regulatory compliance across global markets.
Advanced Ready-To-Use Packaging for Parenteral Fill-Finish
We engineer high-performance rtu parenteral packaging kits designed for direct entry into sterile processing environments. Our containment solutions protect pre-sterilized vials, prefilled syringes (PFS), cartridges, and ampoules, ensuring smooth, reliable integration into modern aseptic fill-finish lines.
Strategic Role in Aseptic Drug Delivery
- Bypass Inline Processing: Eliminates the need for inline washing, depyrogenation tunnels, and autoclaving equipment.
- Accelerate Market Timelines: Significantly reduces batch setup times, speeding up clinical trials and commercial production runs.
- Minimize Contamination Risks: Delivered pre-sterilized and particulate-controlled to ensure a robust, reliable container closure system.
Core Product Formats
We supply standard and engineered packaging configurations tailored to handle delicate parenteral containers:
| RTU Format | Structural Design & Application |
|---|---|
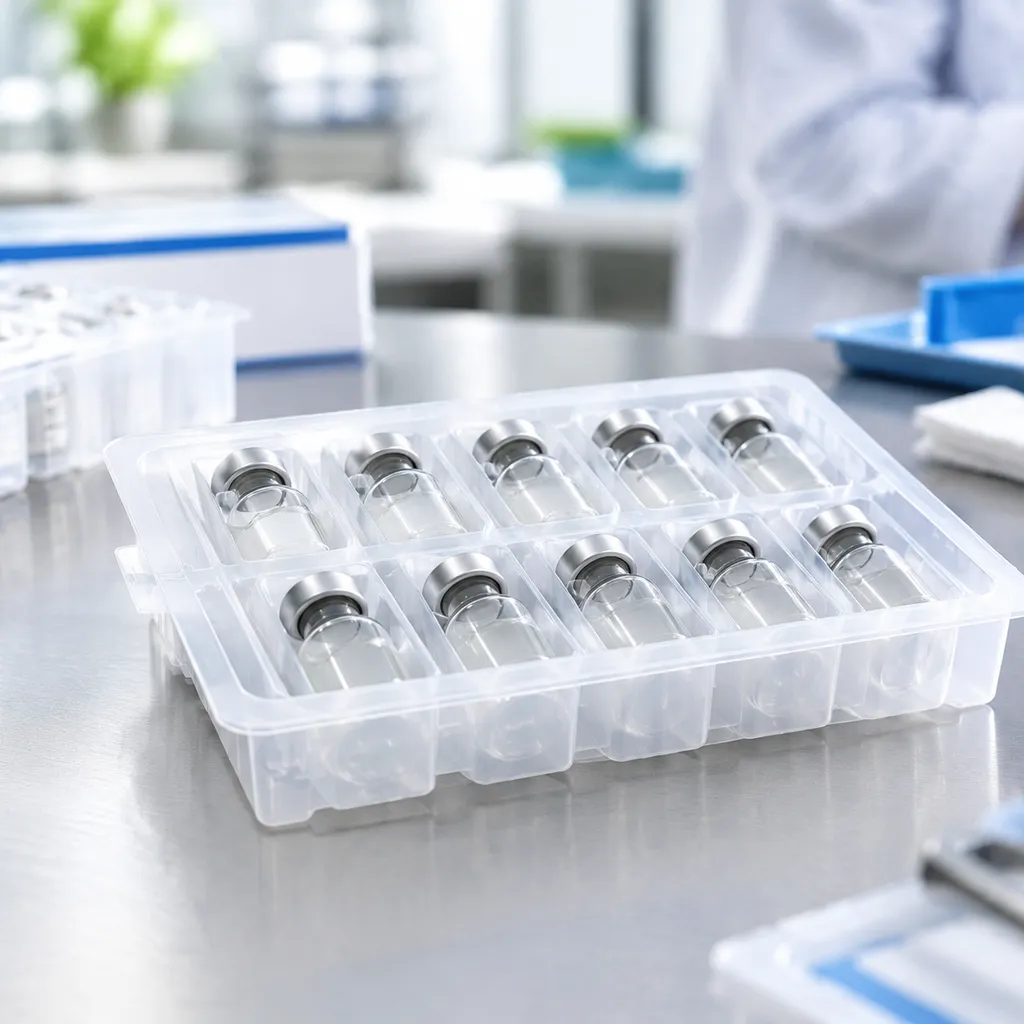
| RTU Nest & Tub Systems for Vials | High-stability matrix nests that eliminate glass-to-glass contact during high-speed filling. |
| Prefilled Syringe (PFS) Trays | Rigid, secure positioning for pre-sterilized barrels to preserve tip seals and prevent flange chipping. |
| Cartridge & Ampoule Trays | Impact-resistant nest geometry designed specifically for auto-injector cartridges and fragile biopharmaceutical ampoules. |
| Custom Trays | Tailored configurations built to package rtu components with non-standard dimensions or custom filling line interfaces. |
Core Operational Advantages & ROI Drivers
We design our rtu pharma kits to tackle the primary operational bottlenecks in modern biopharmaceutical manufacturing: heavy capital expenditure, elevated contamination risks, and line inefficiency.
| Operational Metric | Traditional Processing | Our RTU Pharma Kits |
|---|---|---|
| Capital Infrastructure | Heavy investment in washers & depyrogenation tunnels | Zero inline prep equipment required; direct cleanroom entry |
| Cleanroom Footprint | Expanded footprint with higher utility/maintenance OpEx | Minimal footprint with reduced energy and validation costs |
| Contamination Risk | Elevated risk during manual preparation and transfer | Strict particulate control prevents secondary contamination |
| Filling Line Speed | Prone to handling jams and custom tooling delays | Standardized matrix footprints for automated RABS and Isolators |
Strategic Value for Modern Fill-Finish Lines
- Infrastructure Elimination: Bypassing inline washing, drying, and depyrogenation steps significantly lowers initial cleanroom CapEx and ongoing utility OpEx.
- Contamination Risk Mitigation: Manufactured under stringent particulate and bioburden standards, our pre-sterilized RTU parenteral packaging kits remove human handling steps to prevent secondary contamination in critical aseptic zones.
- High-Speed Automation Integration: Standardized nest-and-tub footprints allow seamless interface with high-speed robotic systems, Isolators, and RABS filling lines for rapid batch changes.
- Optimized Cold-Chain Logistics: High-density nesting configurations hold containers rigidly in place, protecting delicate glass and polymer primary packaging against mechanical shock during cold-chain transport.
Specialized Components in Our RTU Pharma Kits
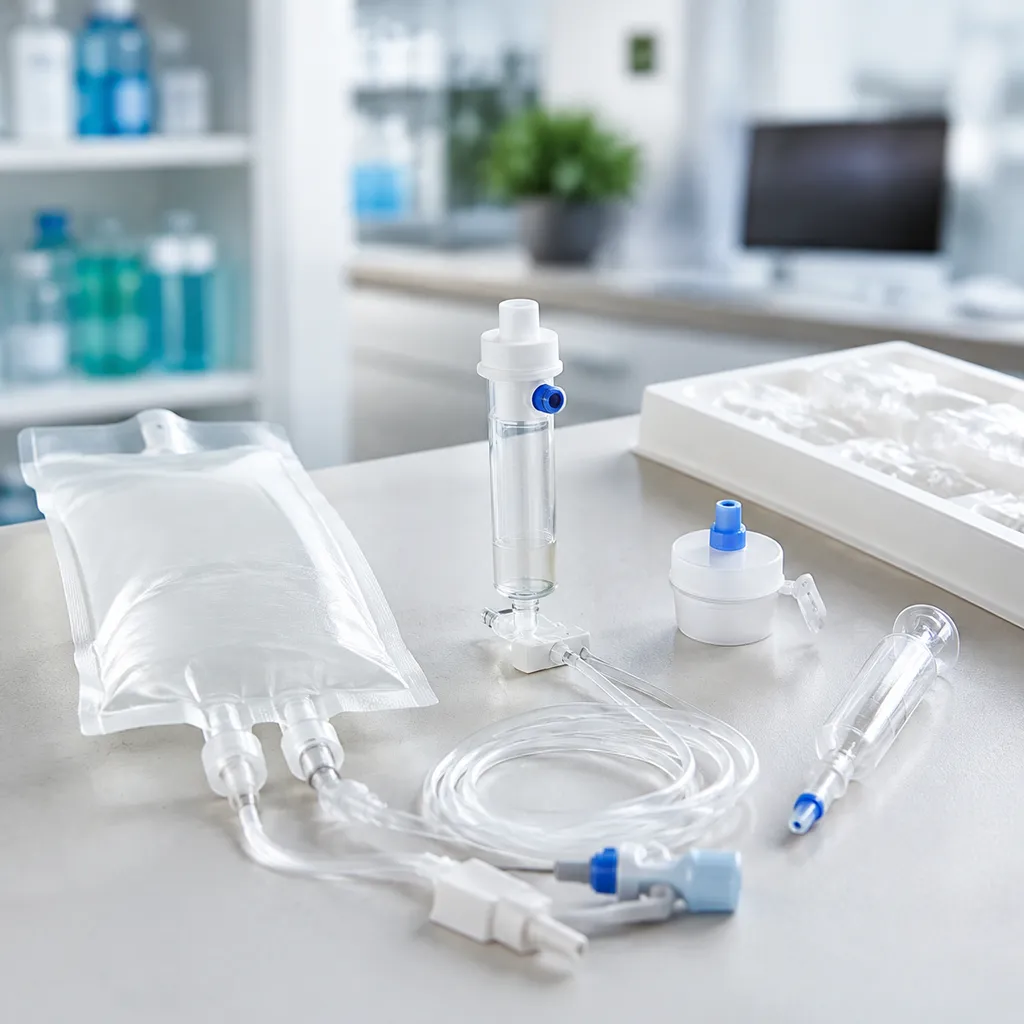
- RTU Nest & Tub Systems for Vials: Rigid, high-stability matrix nests lock each container in an exact position. This layout eliminates glass-to-glass contact on high-speed filling lines, stopping cosmetic scratching, glass breakage, and particulate formation. These systems integrate smoothly with our custom glass vial packaging options for bulk orders.
- Prefilled Syringe (PFS) Containment Trays: Precision-molded positioning slots hold pre-sterilized syringe barrels securely by the shoulder. This firm grip prevents flange chipping, stops accidental plunger movement, and preserves tip seal integrity during high-speed robotic de-nesting.
- Shock-Absorbent Cartridge & Ampoule Trays: Designed with custom nest geometry and impact-resistant support ribs to cushion delicate biopharmaceutical containers. When you package rtu formats for auto-injectors and sensitive biologics, these trays absorb transport shock and vibration, safeguarding high-value filled custom pharmaceutical cartridges for injectable drugs.
Quality Assurance & Compliance for RTU Pharma Kits
Strict Material Integrity & Zero Leachables
- USP Class VI Medical-Grade Polymers: We build our rtu parenteral packaging kits using high-purity materials like COP, COC, and PP to prevent extractables and leachables from compromising active pharmaceutical ingredients (APIs).
- Container Compatibility: Formulated to maintain full structural and chemical stability across diverse vial and ampoule formats under deep-freeze and ambient storage conditions.
Bioburden & Particulate Control
- Cleanroom Manufacturing: Injection molding and assembly occur strictly inside ISO Class 7 and Class 8 cleanroom environments.
- Routine Environmental Monitoring: Continuous particulate counting and bioburden testing guarantee that our rtu pharma kits arrive ready for direct entry into aseptic processing isolators and RABS lines.
Audit-Ready Documentation Package
Every batch ships with a comprehensive compliance folder to fast-track your quality assurance release:
Certificate of Analysis (CoA): Lot-specific test results verifying cleanliness and sterility assurance.
Dimensional Inspection Reports: Precision data confirming exact nest and tub tolerances.
Safety & Material Compliance: Complete Material Safety Data Sheets (MSDS) and raw polymer certificates.
Custom OEM/ODM Engineering & Rapid Prototyping
We engineer custom rtu parenteral packaging kits designed to match your specific container geometries, fill-finish line configurations, and drug product stability requirements.
Engineering Consultation & Technical Alignment
We assess your automated filling line architecture, Isolator/RABS specs, and container contact tolerances before cutting steel. This eliminates downstream handling issues and guarantees exact nest placement.
Precision CAD & Tooling Development
Our engineering team transitions your project from initial 3D models to physical parts with strict precision:
Prototyping: Single-cavity rapid tooling for fit testing and line trials.
Production Molds: High-cavitation tooling built for high-volume production of rtu pharma kits.
Turnaround Timelines
To keep your validation schedule on track, we streamline design and production cycles:
Standard Modifications: 7–10 working days.
Custom Tooling: 2–4 weeks from initial CAD approval to physical sample delivery through our streamlined fast sampling and prototyping workflows.
ISO Cleanroom Manufacturing
Every custom package rtu solution moves directly into automated production within ISO Class 7 and Class 8 cleanroom environments, delivering fully certified, low-particulate packaging ready for direct entry into your sterile fill-finish suite.
Frequently Asked Questions
Can RTU kits be designed for custom or non-standard vial/syringe dimensions?
Yes. We regularly design custom rtu parenteral packaging kits tailored to unique container geometries, non-standard fill volumes, and proprietary filling line specs. Our engineering team handles everything from initial CAD design and rapid prototyping to full-scale production tooling, ensuring seamless integration with your automated isolators or RABS lines.
What polymer materials are recommended for biopharmaceutical RTU trays?
We manufacture our RTU trays using USP Class VI medical-grade polymers selected specifically for biopharmaceutical compatibility and structural protection:
- Cycloolefin Polymer (COP) & Copolymer (COC): Premium choice for high-value biologics, offering glass-like clarity, ultra-low extractables, and exceptional break resistance.
- PETG (Polyethylene Terephthalate Glycol): Excellent balance of clarity, toughness, and chemical resistance for rigid ampoule and medical packaging trays.
- Polypropylene (PP): Ideal for cost-effective structural nests requiring heat resistance and durability during cold-chain transport.
What documentation accompanies custom RTU packaging shipments?
To streamline your incoming quality control and regulatory validation, every batch of our rtu pharma kits includes a complete compliance documentation package:
- Certificate of Analysis (CoA): Confirming bioburden, particulate count, and dimensional integrity against your specs.
- Material Data Sheets (MSDS / SDS): Full raw material safety and origin verification.
- Dimensional Inspection Reports: Optical measurement datasets verifying critical tolerances.
- Lot Traceability Certificates: Complete tracking from raw resin batches to final cleanroom packaging.
Request a Tailored RTU Packaging Proposal
We partner directly with biopharma engineers and procurement teams to design custom rtu parenteral packaging kits built for seamless integration into your aseptic fill-finish lines. Our team provides direct structural design guidance to protect container integrity and streamline high-speed automated handling.
To help us engineer the ideal package rtu solution for your operations, share your target specifications with us:
| Required RFQ Detail | Key Technical Parameters |
|---|---|
| Container Dimensions | Specific height, outer diameter, and flange geometry (vials, PFS, cartridges, ampoules) |
| Material & Polymer Grade | Preferred USP Class VI medical-grade polymers (COP, COC, PP, PETG, PS) |
| Filling Line Architecture | Automated isolators, RABS systems, or custom nest matrix handling setups |
| Volume & Scale | Prototyping quantities, clinical trial batches, or commercial annual volume |
Fast Turnaround & Technical Commitment
We deliver detailed technical responses, CAD recommendations, and price quotes within 12 to 24 hours. Through our dedicated technical support and engineering consultation, we evaluate drug-product sensitivity and filling line requirements upfront to accelerate project timelines.
Whether scaling clinical batches or upgrading commercial lines, our flexible custom RTU packaging solutions ensure your high-value rtu pharma kits arrive pre-sterilized, compliant, and ready for immediate production.
Related Sources
- https://imagroup.com/insights/managing-ready-to-use-rtu-containers-in-aseptic-production-facilities-a-path-to-efficiency-and-compliance/
- https://www.cormica.com/services/physical-and-packaging-testing/physical-mechanical-testing-for-medical
- https://www.cormica.com/services/physical-and-packaging-testing/physical-mechanical-testing-for-medical-devices/iso-11040-prefilled-syringe-testing-standards/