Formula details
Product Details
Overview
Key Value Drivers of Prefilled Syringe Trays
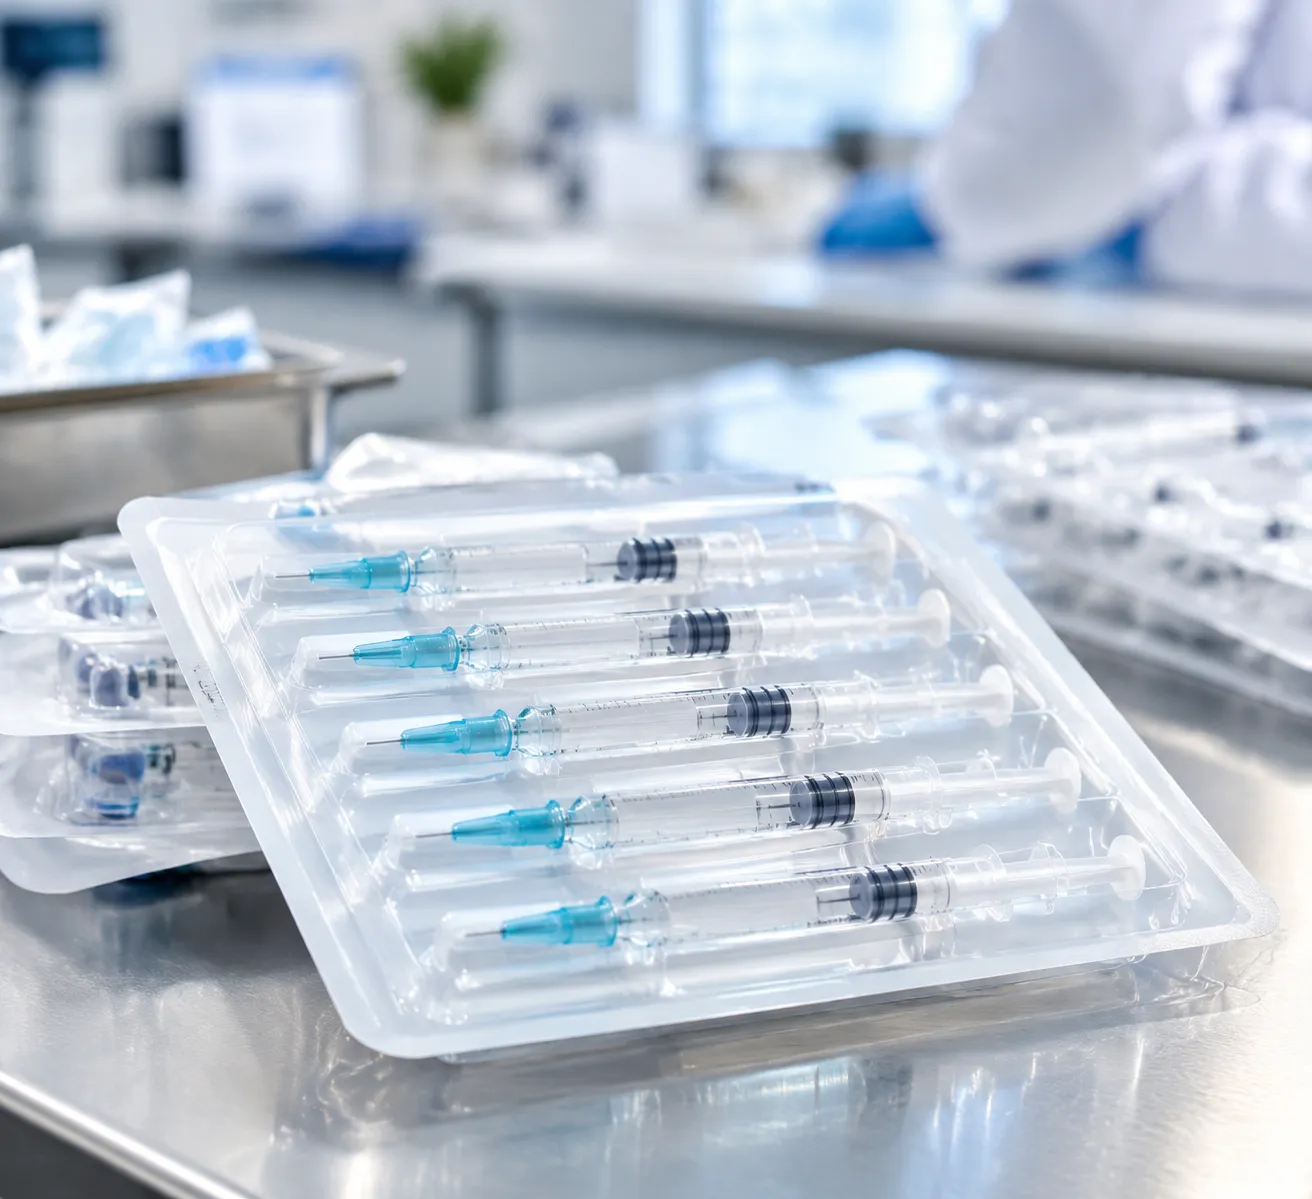
We engineer our prefilled syringe trays to eliminate automated line stoppages, prevent glass-to-glass contact, and protect drug sterility throughout high-volume processing and transit. Every tray is built to solve the core mechanical and regulatory friction points faced by pharmaceutical packaging engineers and fill-finish teams.
Zero-Particulate Cleanroom Manufacturing
Particulate contamination compromises drug safety and triggers batch rejections. We produce all thermoformed prefilled syringe packaging inside certified ISO Class 7 and Class 8 cleanrooms with strict bioburden and static controls.
- Electrostatic Dissipation: In-line anti-static deionization neutralizes surface charges during forming, preventing airborne particulate attraction.
- Non-Shedding Materials: High-purity medical polymers eliminate particulate shedding, plastic flaking, and dust during de-nesting and shipping.
- Continuous Particulate Monitoring: In-process optical scanning confirms low bioburden levels compliant with injectable drug release criteria.
High-Speed Automation and Anti-Jam De-Nesting
Automated filling lines require uninterrupted tray handling. We integrate precision anti-jam de-nesting lugs and uniform draft angles directly into our mold tooling to guarantee seamless robotic separation.
- Engineered De-Nesting Lugs: Calibrated stacking shoulders prevent secondary vacuum lock between nested trays.
- Vacuum Pick-and-Place Pads: Flat surface land zones allow standard suction cups to transfer trays at speeds exceeding 300 units per minute.
- Dimensional Repeatability: Tight thermoforming tolerances ensure consistent integration into automated feed magazines and blister sealing units without jamming.
Impact-Resistant Cavity Geometry
Glass syringes, staked needles, and extended finger flanges are vulnerable to vibration and drops. Our cavity geometries provide dedicated retention zones that secure the syringe body while isolating delicate components.
- Flange Immobilization: Form-fit recesses trap both cut and round glass flanges, preventing rotational and axial movement.
- Rigid Needle Shield (RNS) Clearance: Dedicated suspended pockets isolate the needle tip and RNS from physical contact, eliminating the risk of accidental activation or bent needles.
- Plunger Rod Dampening: Continuous support ribs absorb side-impact shocks and prevent accidental plunger displacement during secondary distribution.
Regulatory Standards Matrix
We align our manufacturing environments, raw resin sourcing, and quality management systems with global medical and pharmaceutical packaging standards.
| Standard / Regulation | Compliance Scope | Operational Verification |
|---|---|---|
| ISO 13485:2016 | Medical device packaging quality systems | Certified full-lifecycle QMS audit trail |
| FDA 21 CFR Part 211 / 820 | cGMP packaging validation & traceability | Lot-specific Certificates of Analysis (CoA) |
| USP Class VI | Biological reactivity and resin biocompatibility | Certified raw polymer lot extraction testing |
| ISO 14644-1 (Class 7/8) | Cleanroom environment controls | Real-time airborne particle count verification |
| USP <788> | Particulate matter in injections | Microscopic and light obscuration testing |
Technical Specifications and Material Options for Prefilled Syringe Trays
Syringe Format and Dimensional Specifications
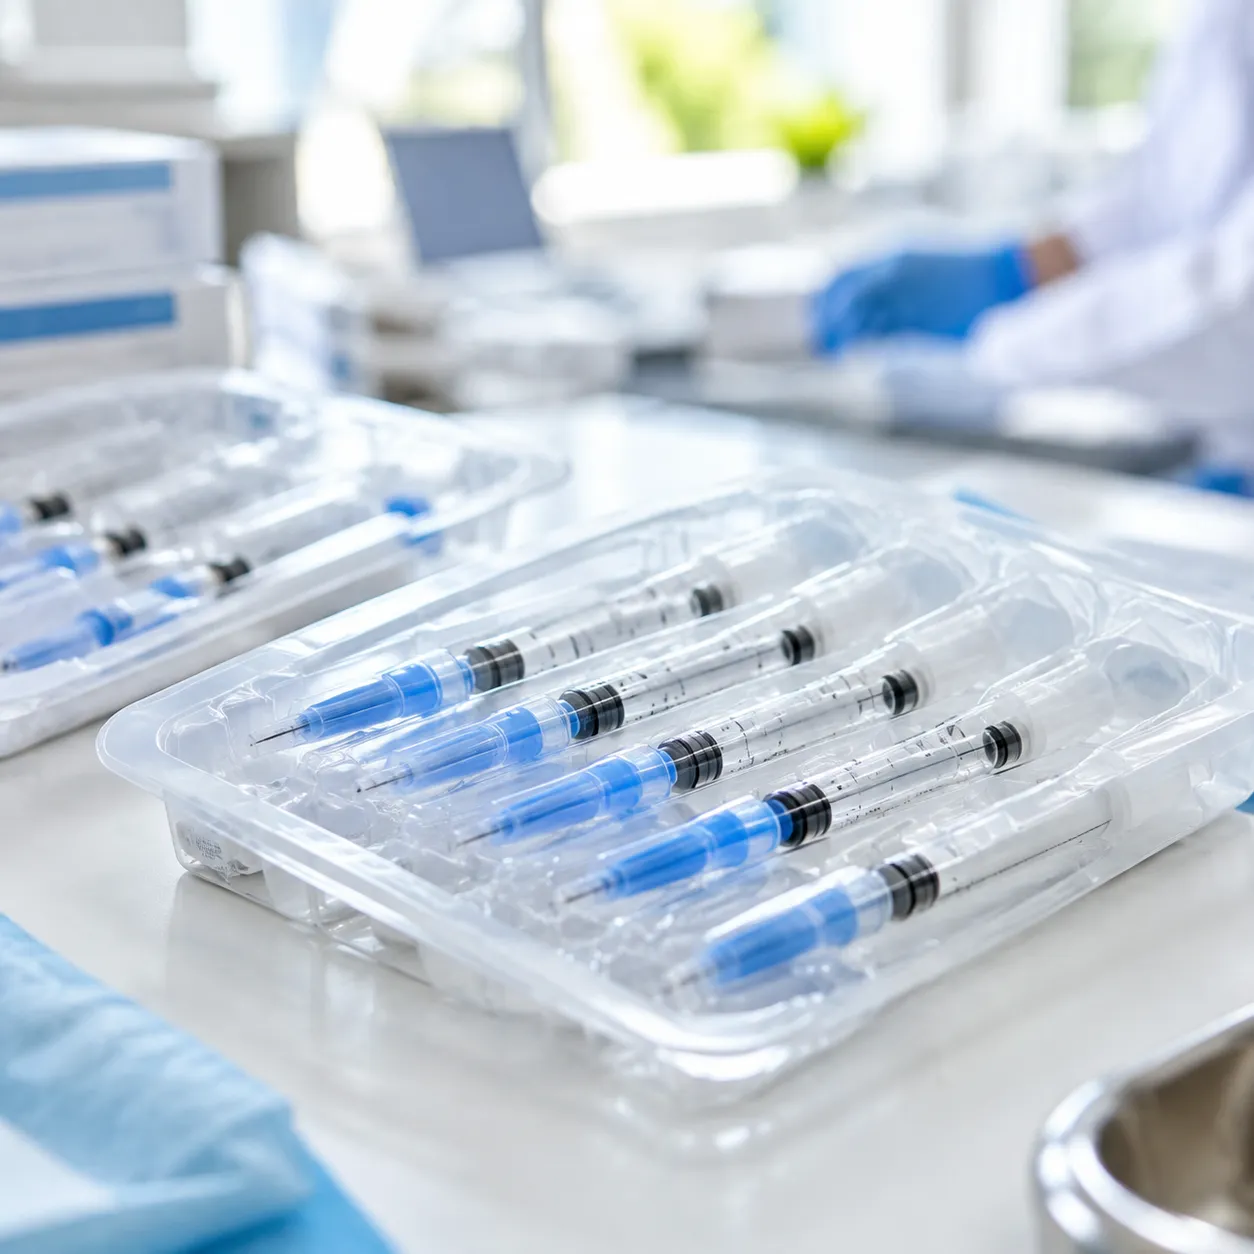
We design custom nests and blisters for standard glass and cyclic polymer barrels across all global fill volumes:
- Syringe Capacities: 0.5 mL, 1.0 mL (Standard & Long), 2.25 mL, 3.0 mL, 5.0 mL, 10 mL, and 20 mL.
- Tip Configurations: Staked needle (with RNS/rigid needle shields), Luer Slip, and Luer Lock (with tip caps).
- Gauge Clearances: Full cavity clearances designed for 27G to 31G ultra-thin needles.
- Sheet Thickness Range: 0.40 mm to 1.50 mm (16 mil to 60 mil).
- Tooling Precision: Strict dimensional tolerances held within ±0.1 mm for seamless pick-and-place automation.
| Parameter | Specification / Range | Compliance & Standards |
|---|---|---|
| Material Thickness | 0.40 mm – 1.50 mm (Customizable) | ASTM D374 |
| Forming Precision | ±0.1 mm | ISO 9001 / ISO 13485 |
| Syringe Compatibility | 0.5 mL to 20 mL (Glass & COC/COP) | ISO 11040-4 / ISO 11040-6 |
| Sterilization Suitability | EtO, Gamma (25–50 kGy), E-Beam, Autoclave | ISO 11135 / ISO 11137 |
Medical-Grade Substrate Selection
Choosing the proper medical-grade packaging materials for sterility and barrier performance is critical to prevent chemical leaching and ensure seal integrity. We thermoform prefilled syringe packaging using fully certified resins:
- Medical-Grade PETG: High clarity, excellent impact toughness, and broad sterilization compatibility (EtO and Gamma). Ideal for staked needle syringe holding trays.
- APET: Cost-effective, rigid secondary packaging solution for non-radiation sterilized products.
- Conductive / Anti-Static HIPS: Surface resistivity of $10^6$ to $10^9$ ohms/sq, eliminating ESD risks and particulate attraction on automated packaging lines.
- Polypropylene (PP): Autoclave-compatible polymer providing high chemical resistance and cost efficiency.
- COC / COP: Ultra-low moisture absorption and exceptional clarity for sensitive biologics and high-potency drugs.
Lidding and Heat-Seal Compatibility
We configure our flange surfaces to guarantee sterile barrier formation. All thermoformed syringe blister packaging trays provide uniform heat distribution for rapid sealing cycles:
- Tyvek Lidding: Compatible with DuPont Tyvek 1073B, 1059B, and 2FS breathable webs for EtO gas permeation.
- Aluminum Foil Laminates: High-barrier, peelable, and push-through foil structures for complete light and moisture barriers.
- Coating Adhesion: Engineered to bond with water-based, solvent-based, or hot-melt heat-seal coatings without fiber tear or channel leaks.
Precision Engineering and Cavity Design Features
High-speed fill-finish operations and automated packaging lines leave zero margin for loose tolerances. We engineer our thermoformed prefilled syringe packaging with dedicated cavity geometries that immobilize the syringe body while isolating critical sterile barriers from impact and surface contact.
Precision PFS Cavity Design Profile
Plunger Support
→ Prevents plunger dislodgement
↓
Flange Lock
→ Prevents axial movement
↓
Suspended Barrel Support
→ Minimizes barrel contact and friction
↓
RNS / Tip-Cap Clearance
→ Zero-touch recessed zone
Critical Cavity Architecture
- Flange and Finger Grip Locking Mechanisms: Precision undercut detents snap securely beneath the syringe flange (supporting both cut and round flange formats). This design locks the glass barrel in place, eliminating axial play and preventing glass-to-plastic abrasion during secondary transport.
- Plunger Rod and Backstop Support: Molded end-stops seat the plunger rod and optional backstops. This rigid retention prevents accidental forward depression—eliminating product leakage—and stops backward travel that could compromise sterile boundary seals.
- Tip-Cap and Rigid Needle Shield (RNS) Clearance: Deep-draw suspended pockets keep the RNS or Luer tip-cap completely free from cavity floor contact. By isolating the closure, we eliminate micro-abrasions, closure loosening, and needle tip blunting.
- Automation De-Nesting Lugs and Pick-and-Place Chamfers: Engineered stacking shoulders ensure exact stack pitch and prevent vacuum locks between nested units. Much like our vial nest and tub system for RTU aseptic fill-finish, the thermoformed lead-in chamfers ensure reliable, continuous feeding on high-speed robotic de-nesters and pick-and-place end effectors.
- High-Density Nesting Ratio: Tapered outer draft angles maximize nesting density when stacked empty. This tight nesting ratio reduces cleanroom staging footprint by up to 40% and significantly lowers international freight costs.
Cavity Engineering Specifications
| Design Element | Engineering Focus | Functional Benefit |
|---|---|---|
| Flange Undercuts | Snap-retention ribs | Eliminates syringe rotation and axial rattle |
| Plunger Lockouts | Longitudinal barrier rib | Prevents unintentional drug discharge and stopper displacement |
| RNS Relief Wells | Suspended deep-draw pocket | Maintains sterile closure integrity with zero friction |
| Anti-Jam De-Nesting Lugs | Calibrated stack-offset ledges | Guarantees single-tray dispensing on automated packaging lines |
| Perimeter Chamfers | Lead-in guide angles | Enables seamless vacuum pick-and-place transfer |
Sterilization Compatibility and Regulatory Compliance for Prefilled Syringe Trays
Validated Sterilization Profiles
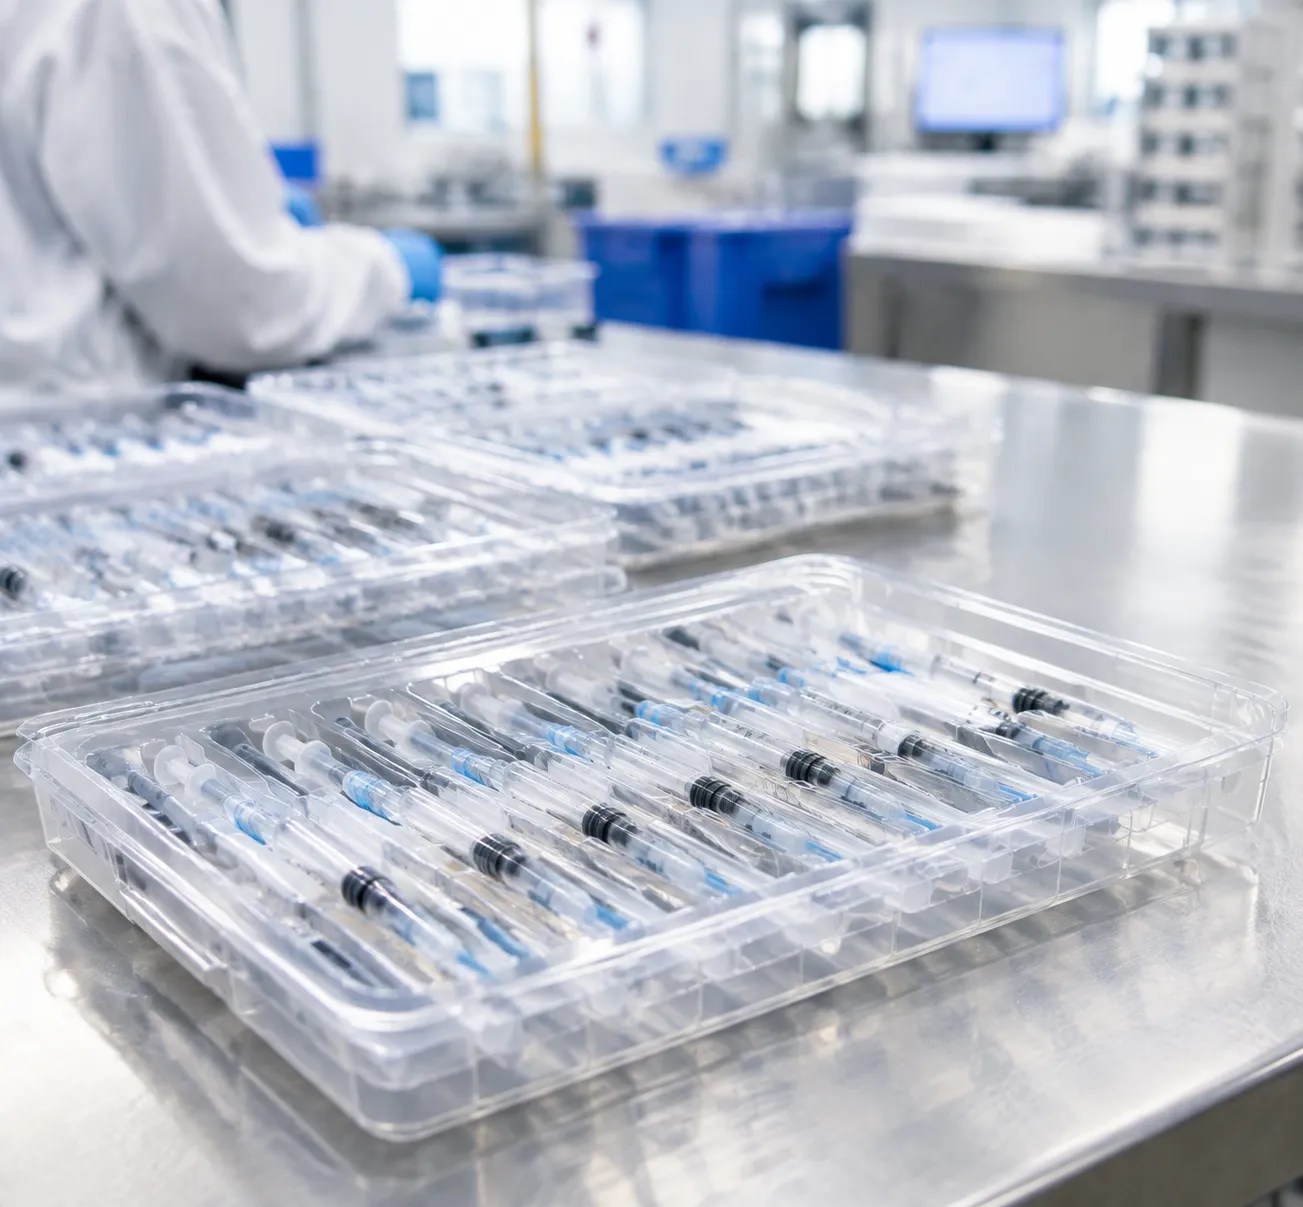
Our thermoformed prefilled syringe packaging supports multiple terminal sterilization methods depending on your selected polymer substrate:
- Ethylene Oxide (EtO): Compatible with medical-grade PETG, APET, and COC/COP trays paired with breathable Tyvek lidding. Designed to withstand standard gas diffusion and degassing phases without warping.
- Gamma & E-Beam Radiation: High-energy beam compatibility using radiation-stabilized PETG and specialized PP formulations (validated up to 50 kGy) with zero yellowing or polymer embrittlement.
- Steam Autoclave: High-heat polypropylene (PP) formulations built to maintain structural cavity shape under 121°C moist-heat cycles.
| Sterilization Method | Recommended Substrates | Max Temperature / Dose | Key Advantage |
|---|---|---|---|
| EtO Gas | PETG, APET, COC/COP | 55°C – 60°C | Excellent gas permeability with Tyvek |
| Gamma Radiation | Radiation-Grade PETG, PP | 25 – 50 kGy | Deep penetration for sealed RTU formats |
| E-Beam | PETG, PP, Barex alternatives | 25 – 45 kGy | Fast throughput, minimal polymer stress |
| Steam Autoclave | Medical Polypropylene (PP) | 121°C (15–30 min) | High heat tolerance, chemical inertness |
Cleanroom Thermoforming and Quality Control
We operate certified ISO Class 7 (Class 10,000) and ISO Class 8 cleanrooms to manufacture our nested tub and tray aseptic processing solutions, minimizing initial bioburden and airborne particulate risks before downstream filling operations.
- Particulate Monitoring: Continuous airborne particle counters and liquid particle testing compliant with USP <788> standards.
- Bioburden & Sterility Assurance: Routine bioburden microbial profiling in accordance with ISO 11737-1 to ensure low pre-sterilization bio-loads.
- Residual Solvent & Extractables Testing: Gas Chromatography-Mass Spectrometry (GC-MS) screening to guarantee zero chemical leachables or toxic solvent residues.
Full Lot Traceability and Documentation
Every production run of our ISO 13485 syringe packaging includes a comprehensive documentation pack:
- Certificates of Analysis (CoA) & Conformity (CoC): Validating resin melt flow index, sheet gauge tolerance, and mechanical impact thresholds.
- End-to-End Batch Traceability: Unbroken tracking linking raw medical-grade resin lots to cleanroom extrusion, thermoforming runs, visual inspection, and final palletized inventory.
- Regulatory Compliance: Raw materials fully certified to meet USP Class VI, FDA 21 CFR 177.1630, EU 10/2011, and EP 3.1.2 standards.
Pharmaceutical and Biotech Applications for Prefilled Syringe Trays
Ready-to-Use (RTU) Vaccine and Biologics Containment
High-value biologics and temperature-sensitive vaccines demand zero-particulate integrity and dimensional stability under cold-chain storage (down to -80°C).
Zero Contamination: Manufactured in ISO Class 7 cleanrooms to comply with stringent particulate and bioburden standards.
Cold-Chain Durability: Custom medical-grade PETG and cyclic olefin copolymers (COC) prevent low-temperature embrittlement and tray warping during storage.
Optimized RTU Formats: Compatible with standardized tub-and-nest setups for automated high-speed aseptic filling lines.
Hyaluronic Acid and Dermal Filler Packaging
Aesthetic injectables require high clarity for visual inspection alongside secure cavity geometry to lock heavy, viscous-filled glass barrels in place.
Flange & Plunger Protection: Engineered snap-in detents keep pre-assembled luer lock syringes completely immobilized.
Needle & Accessory Cavities: Custom multi-cavity layouts securely hold prefilled syringes alongside disposable hypodermic needles and backstops.
Premium Shelf Presentation: Crystal-clear pharmaceutical syringe blister packaging allows full product visibility while maintaining a rigid sterile barrier when sealed with Tyvek lidding.
Anticoagulant (Heparin & Enoxaparin) Syringe Handling
High-volume anticoagulant packaging requires ultra-reliable de-nesting and high-impact shock absorption for high-speed secondary packaging lines.
Needle Shield Recesses: Deep-draw tip cavities protect rigid needle shields (RNS) and staked needle covers from lateral impact, eliminating needle bending and fluid leakage.
Anti-Static Performance: Anti-static surface treatments prevent electrostatic discharge (ESD) and particle attraction during automated pick-and-place indexing.
| Drug Application | Syringe Size / Type | Key Cavity Feature | Primary Material Substrate |
|---|---|---|---|
| Vaccines & Biologics | 0.5 mL – 1.0 mL Long (Staked Needle) | Rigid needle shield isolation & tub-nest stacking | Medical-Grade PETG / COC |
| Dermal Fillers (HA) | 1.0 mL – 3.0 mL (Luer Lock) | Extended finger grip detents & accessory slots | High-Clarify PETG / APET |
| Anticoagulants | 0.5 mL – 1.0 mL (Staked Needle) | Anti-jam de-nesting lugs & side-flange retention | Conductive / Static-Dissipative HIPS |
| Auto-Injectors | 1.0 mL – 2.25 mL (Sub-Assemblies) | Dual-depth pockets for power packs & safety sleeves | High-Impact Polypropylene (PP) |
Combination Products and Auto-Injector Sub-Assembly Trays
As drug-device combination products expand, we manufacture custom cavity PFS plastic inserts that house both the primary syringe barrel and sensitive electromechanical or spring-loaded auto-injector components.
Modular Multi-Component Layouts: Houses syringe barrels, drive mechanisms, needle safety guards, and plungers in a single organized insert.
Robotic Pick-and-Place Precision: Dimensional tolerances maintained within ±0.1 mm to ensure robotic vacuum grippers can seamlessly load sub-assemblies without mechanical jams.
Secondary Clinical and Commercial Packaging Lines
We engineer comprehensive secondary packaging for syringes designed to streamline the transition from primary sterile processing to secondary boxing, cartoning, and global shipping.
Anti-Shingling & Anti-Jam Stacking: Engineered perimeter de-nesting lugs prevent tray interlock during robotic destacking.
Universal Heat-Seal Flanges: Flat, uniform sealing perimeters ensure 100% seal integrity when applying Tyvek, foil, or medical paper lidding.
Scalable Turnkey Tooling: Rapid prototype sampling for clinical trials transitioning directly to high-cavitation production molds for global commercial rollouts.
Custom OEM/ODM Engineering and Manufacturing Workflow
We build custom prefilled syringe trays tailored to exact drug delivery device tolerances, fill-finish robotics, and secondary packaging lines. Our end-to-end OEM/ODM workflow takes your syringe dimensions from initial concept to commercial-scale cleanroom thermoforming with zero production bottlenecks.
| Stage | Process Focus | Deliverables & Turnaround |
|---|---|---|
| 1. 3D CAD & Interface Analysis | Syringe clearance, flange locking, and de-nesting design | 3D models, DFM report (24–48 hours) |
| 2. Rapid Prototyping | CNC-machined sample molds for functional testing | Physical thermoformed samples (3–5 days) |
| 3. Multi-Cavity Tooling | Aircraft-grade aluminum production mold fabrication | High-cavitation production tooling |
| 4. Cleanroom Thermoforming | ISO Class 7/8 molding with in-line vision inspection | High-speed, particulate-controlled output |
| 5. Cleanroom Packout | Double-poly vacuum sealing with complete lot trace | Validated, cleanroom-ready shipping units |
Technical CAD Review and 3D Syringe Interface Analysis
We start by reviewing your specific syringe specifications—including barrel outer diameter, flange width, extended plunger rod length, and rigid needle shield (RNS) geometry. Our engineering team conducts digital 3D tolerance and interference analysis to guarantee:
Secure finger-flange snap-fits that eliminate axial syringe migration.
Precise clearances around tip caps to prevent seal compromise during shipping.
Automation-friendly profiles aligned with high-speed pick-and-place grippers and automated downstream operations described in our vial packaging process guide for pharmaceutical lines.
Rapid Prototyping and CNC Sampling in 3 to 5 Days
We eliminate long design lead times by cutting prototype tooling on dedicated high-speed CNC milling centers.
Fast verification: Receive thermoformed prefilled syringe packaging prototypes in medical-grade PETG or anti-static HIPS within 3 to 5 business days.
Fit and functional trials: Run physical fit trials with your automated de-nesters, sealing equipment, and secondary cartoning equipment before approving steel or hardened aluminum production molds.
Multi-Cavity Tooling for High-Volume Repeatability
Once samples are approved, we build hardened multi-cavity aluminum tooling with integrated water-cooling channels. This ensures uniform material distribution, strict dimensional stability (±0.1 mm precision), and flat, warp-free sealing flanges across millions of custom cavity PFS plastic inserts.
Cleanroom Thermoforming with In-Line Vision Inspection
We form all pharmaceutical syringe blister packaging inside certified ISO Class 7 and Class 8 cleanrooms.
Automated continuous monitoring: High-resolution optical vision systems inspect 100% of the web for sub-visible particulates, pinholes, flange deformations, and dimensional flaws.
Bioburden mitigation: Continuous HEPA filtration and static neutralization eliminate airborne particulates and electrostatic attraction throughout forming and cutting.
Double-Bag Vacuum Sealing for Cleanroom-Ready Transport
Finished RTU syringe trays pass directly from the cutting station into cleanroom packout.
Trays are stacked using precision anti-nesting lugs to prevent interlocking.
We vacuum-seal nested stacks inside double-layer medical polyethylene bags with lot-traceable indicator labels.
Your operations team can wipe down and transfer outer packaging directly into pharmaceutical cleanroom airlocks without introducing external contaminants.
Frequently Asked Questions About Prefilled Syringe Trays
Line Integration for High-Speed Bosch, Syntegon, and IMA Equipment
Our thermoformed prefilled syringe packaging integrates directly into automated fill-finish and secondary packaging lines. We manufacture each tray with precise perimeter tolerances of ±0.1 mm, engineered de-nesting lugs, and vacuum-assist pick-and-place chamfers to prevent line jams and downtime on high-speed Bosch, Syntegon, IMA, and Schubert systems.
Medical-Grade PETG vs. Standard HIPS for PFS Formats
The choice between medical-grade PETG and conductive or standard HIPS depends on your drug contact requirements, clarity needs, and sterilization method. For applications requiring high clarity alongside products like our ampoule packaging tray and custom PETG medical trays, PETG serves as the pharmaceutical industry benchmark.
| Specification Feature | Medical-Grade PETG | Anti-Static / Standard HIPS |
|---|---|---|
| Optical Clarity | Crystal clear (high transparency) | Opaque (white, blue, or black) |
| Sterilization Profile | EtO, Gamma, E-Beam | EtO, E-Beam |
| Particulate Shedding | Ultra-low / Zero particulate | Low to moderate |
| Primary Use Case | Direct sterile barrier blisters | Secondary shipping & assembly nests |
| Biocompatibility | USP Class VI & ISO 10993 certified | Technical grade / Non-contact grade |
Sealing Machine and Tyvek Lidding Compatibility
We design our Tyvek heat-sealable syringe blisters with continuous, ultra-flat perimeter sealing flanges. They form consistent, sterile peel seals with standard DuPont Tyvek (1073B, 1059B, 2FS) and medical-grade aluminum foil laminates across rotary, shuttle, and continuous inline heat-seal packaging machinery.
Included Regulatory and Validation Documentation
Every production lot of our ISO 13485 syringe packaging includes a comprehensive validation and compliance dossier to streamline pharmaceutical audits:
Certificate of Analysis (CoA): Dimensional verification, residual monomer, and seal-plane flatness checks.
Certificate of Conformance (CoC): Statement of compliance with FDA 21 CFR and cGMP standards.
Biocompatibility Reports: USP Class VI, ISO 10993-5 (cytotoxicity), and ISO 10993-10 compliance data.
Cleanroom Testing Data: Particulate monitoring records (ISO Class 7 / Class 8) and bioburden evaluation metrics.
Traceability Records: Complete resin batch tracking from virgin polymer supply through to final packed carton.
Standard Tooling and Production Lead Times
We maintain fast turnaround cycles to keep fill-finish lines running on schedule, supporting integrated deployments alongside pre-sterilized RTU vials and modular vial systems:
Technical CAD Interface & 3D Modeling: 24 to 48 hours.
CNC Sample Tooling & First-Article Prototypes: 3 to 5 business days.
Multi-Cavity Hardened Production Tooling: 2 to 3 weeks.
High-Volume Cleanroom Production Runs: 10 to 15 business days following final sample sign-off.